


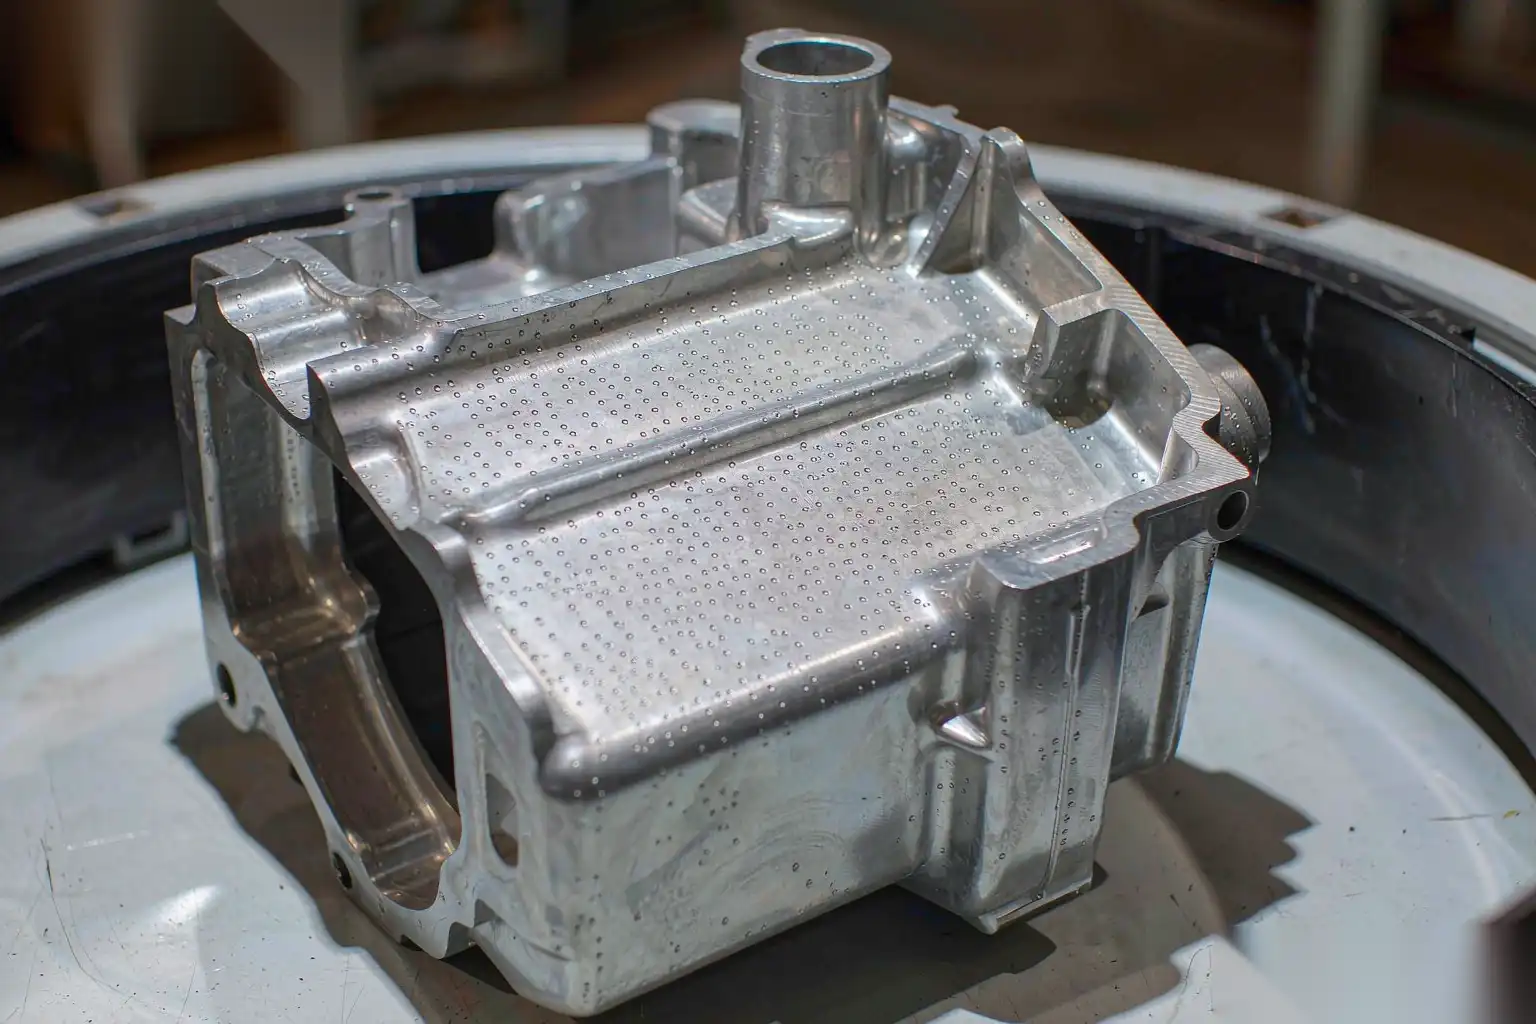
Why ejector pin marks appear, how to relocate and size pins, and how automated polishing handles residual marks.
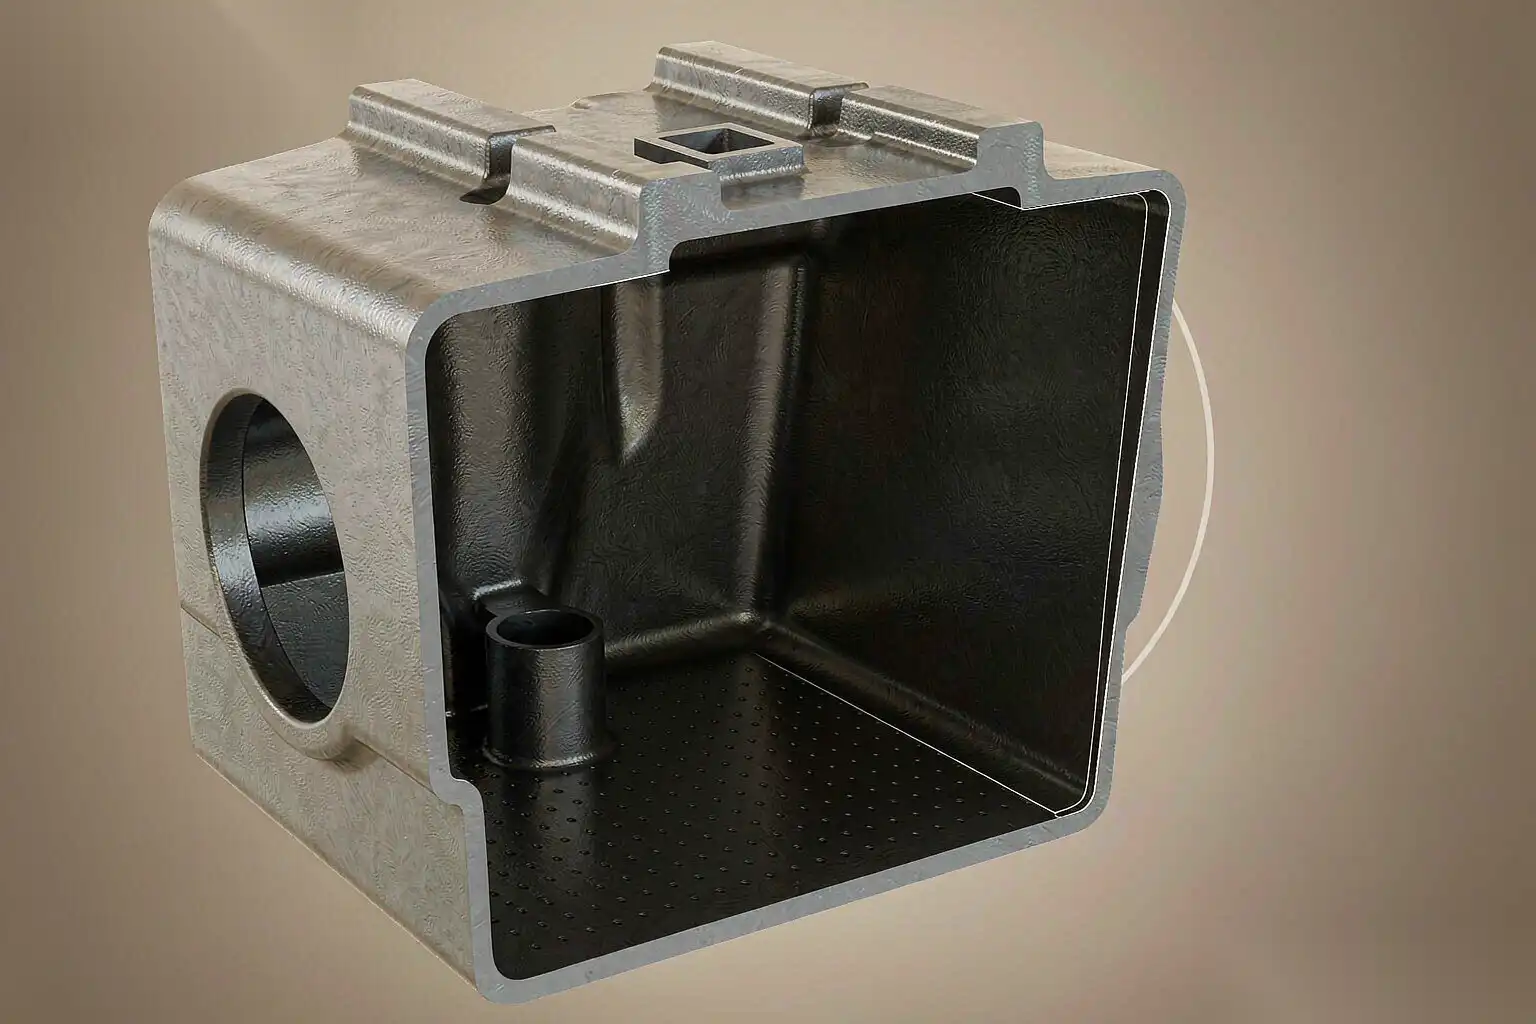
Practical draft angle rules for aluminum die castings, when to add lifters, and how ejection marks affect finishing cost.
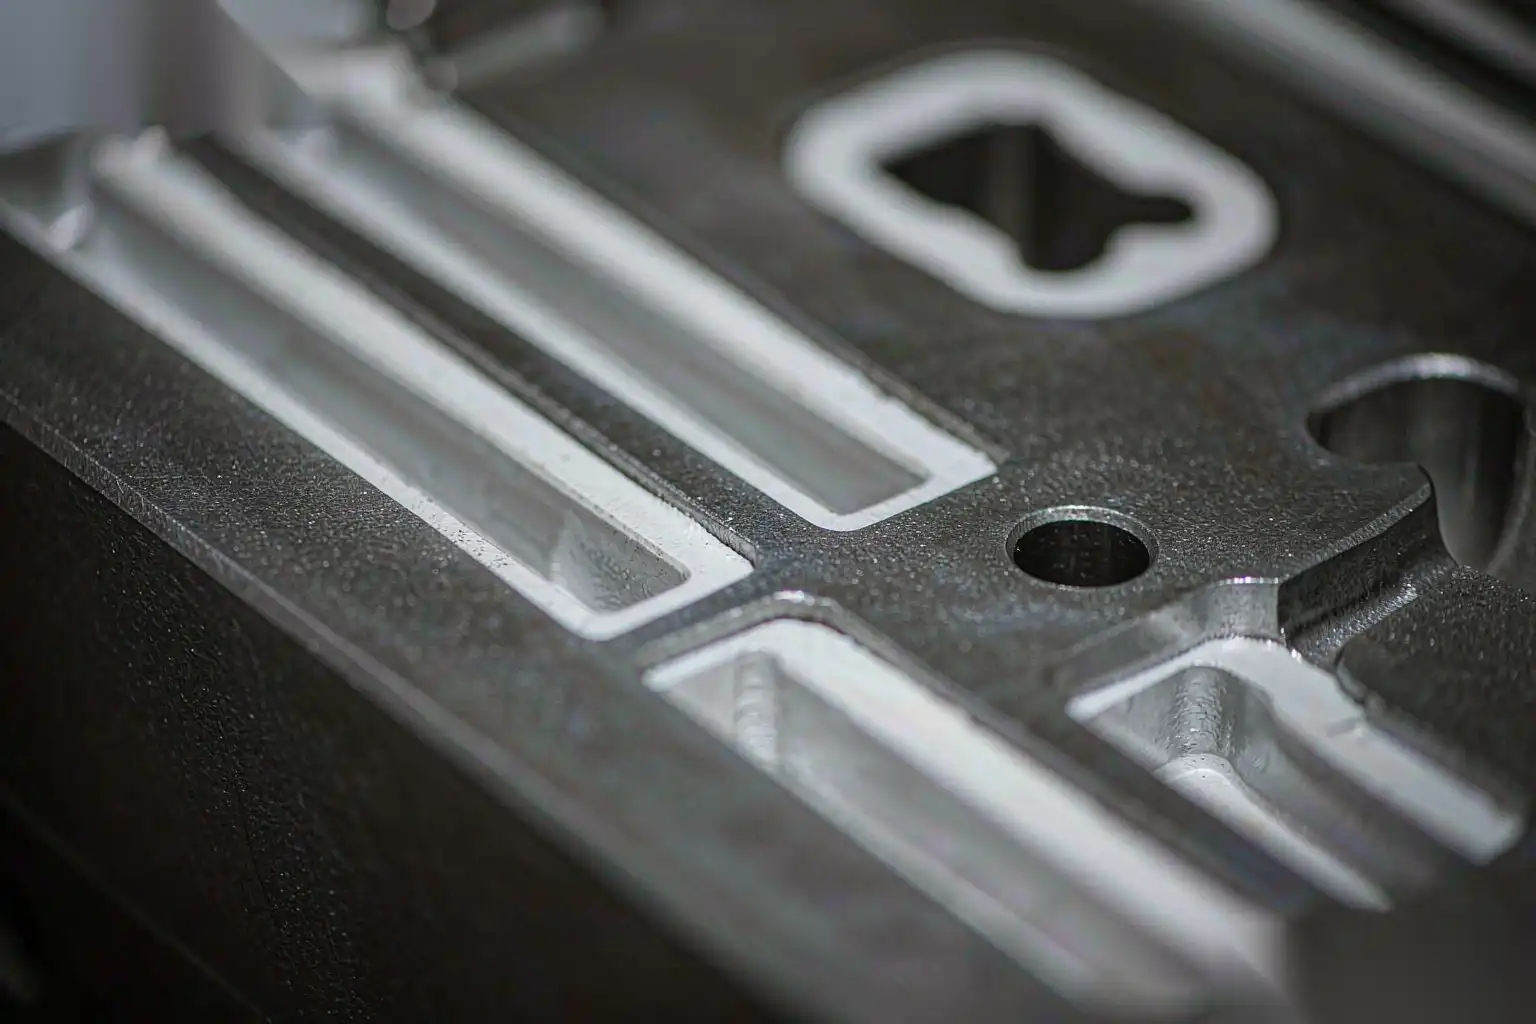
Vent placement, depth and exhaust channels that reduce trapped air, porosity and surface defects on die cast parts.
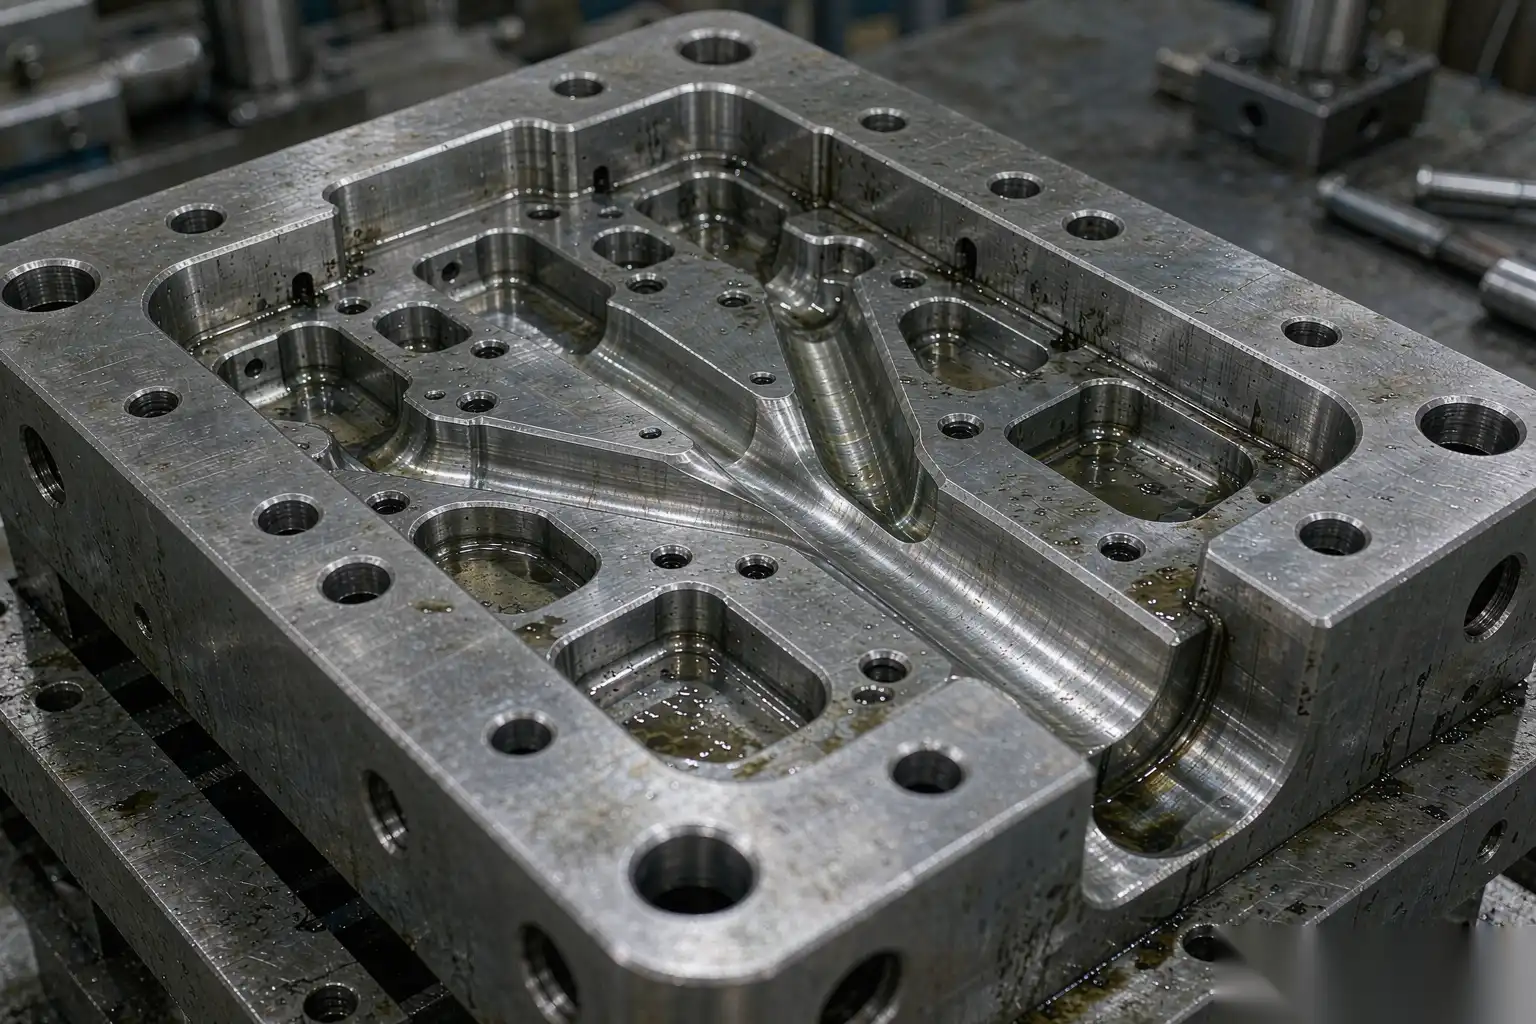
How to design die casting runners, gates and overflows for balanced fill, lower porosity, and easier downstream robotic deburring and polishing.
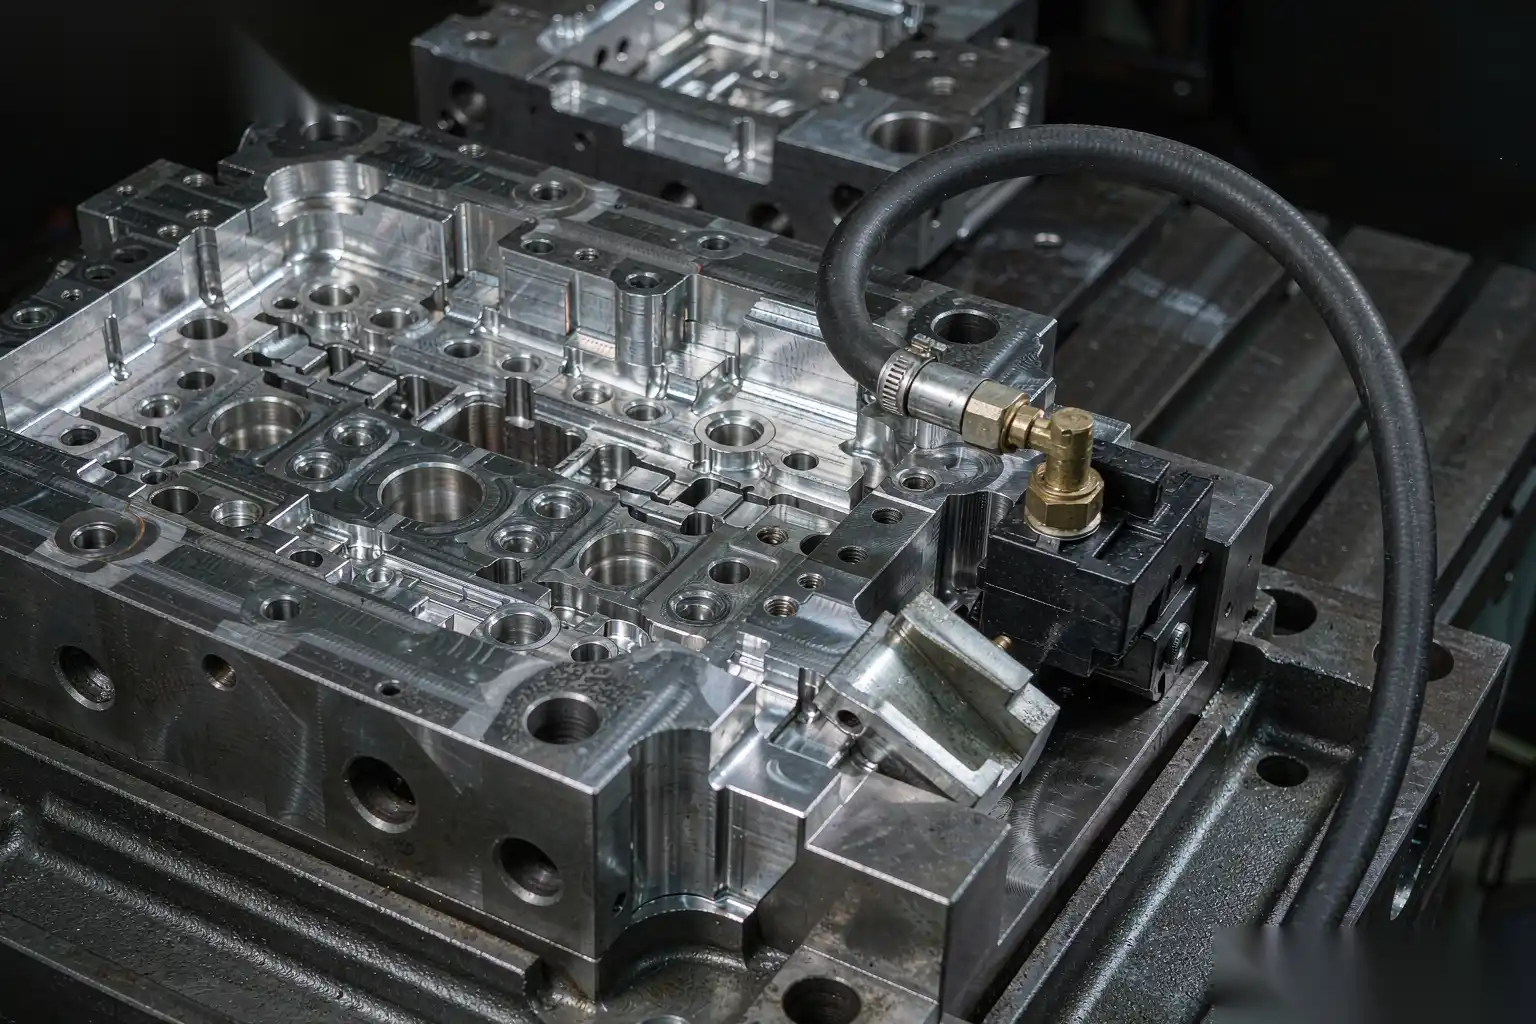
Comparing H13, premium remelted H13, high conductivity and maraging tool steels for die casting: hardness, thermal conductivity, heat checking resistance and cost per shot.
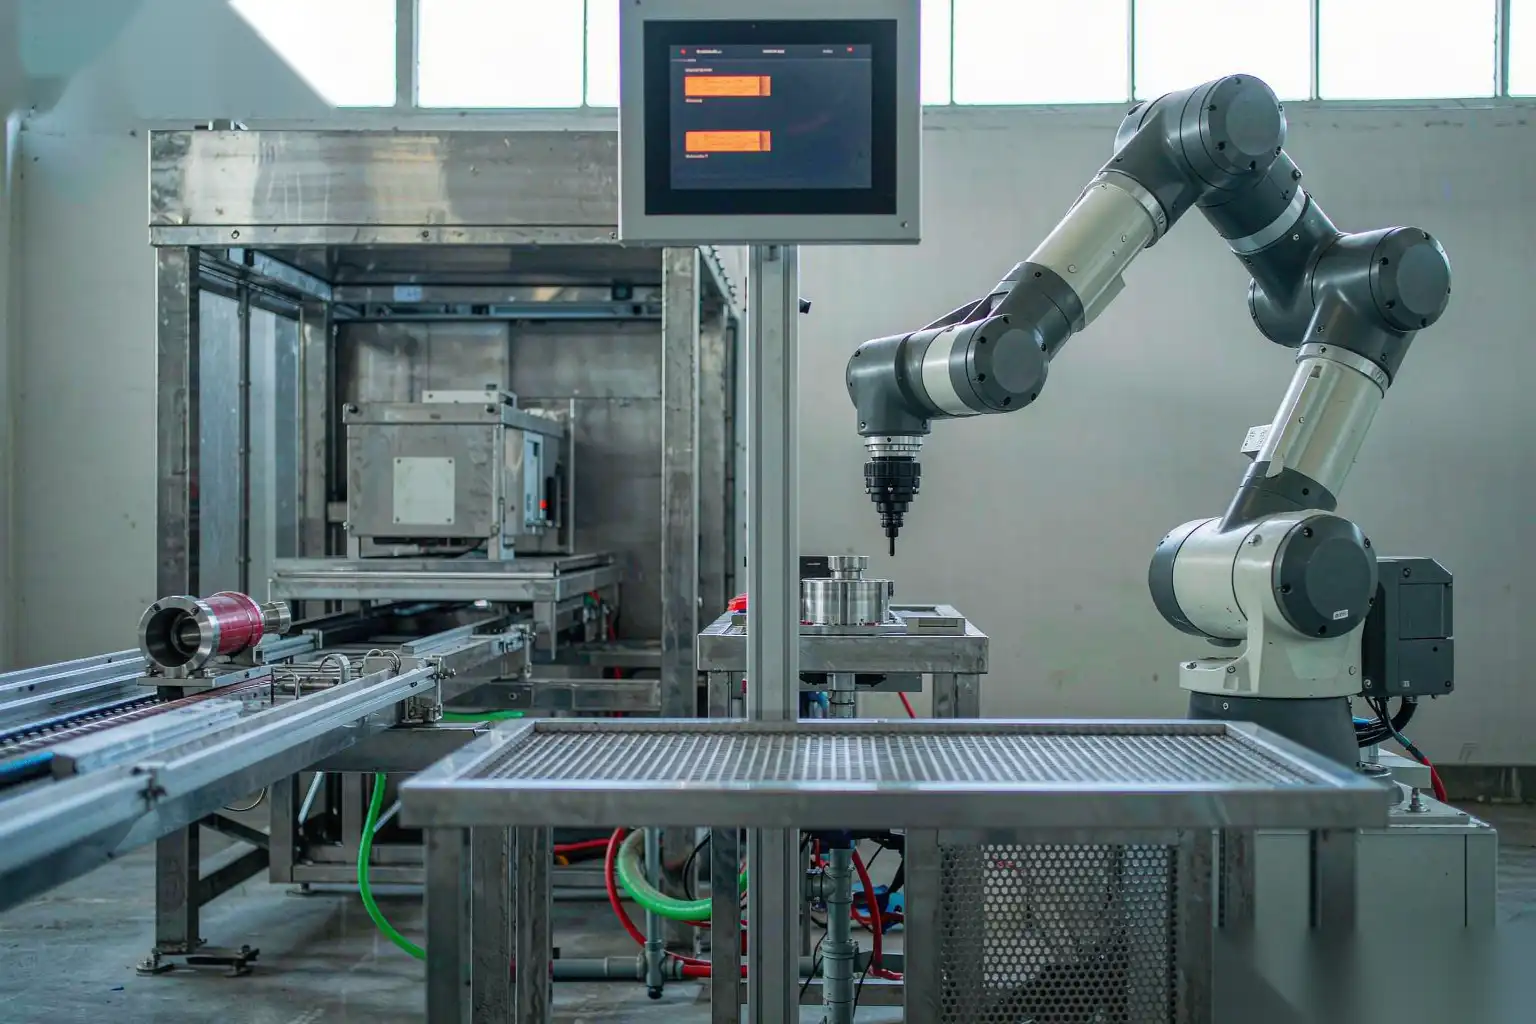
Availability, performance and quality benchmarks for deburring and polishing cells, the downtime causes that dominate, hidden cycle losses, a capture plan and a worked improvement.
BlogDingren Lai2026-09-07T09:54:23+00:00