AT A GLANCE · Surface finish determines how a casting feels, seals, and performs in service. Therefore, understanding the numbers on your print prevents expensive miscommunication between design and production. In this guide we explain surface finish standards Ra Rz and what each value tells you about a real cast part.
The Language of Surface Finish Standards Ra Rz
Engineers describe roughness with a family of profile parameters, but two dominate everyday purchasing and inspection. Ra and Rz are the symbols you see most often on casting drawings across automotive, hydraulic, and medical supply chains. Consequently, specifying one when you mean the other creates avoidable scrap and argument.
DEFINITION — A surface profile parameter is a single number derived from a filtered 2D trace of the part surface, not a direct measurement of every peak and valley.
Defining Ra: Arithmetic Average Roughness
Ra, or roughness average, is the arithmetic mean of the absolute deviations from the mean line within the evaluation length. It smooths the profile into a single representative height value, expressed in micrometers or microinches. Because it averages, Ra is forgiving and easy to compare across parts and suppliers. However, that same averaging hides sporadic deep scratches that may still matter to your seal or coating.
Most castings are quoted against an Ra target because comparators and handheld meters report it directly. Still, the number alone does not tell the whole story of the surface.
Defining Rz: Mean Roughness Depth
Rz measures the average distance between the highest peak and the lowest valley within each of several sampling lengths, then averages those distances. Unlike Ra, it directly captures the extremes of the profile rather than the mean scatter. Consequently, Rz is more sensitive to the occasional deep pit or tear common on as-cast surfaces. European standards historically favored Rz, which is why legacy drawings still call for it.
Because Rz tracks the worst local depth, it correlates better with leak paths and coating adhesion failures. Therefore, specifications that demand sealing or plating often gain more from an Rz limit than from a tight Ra alone.
Ra vs Rz: A Direct Comparison
The table below contrasts how each parameter is calculated, what it emphasizes, and where it fits best.
| Attribute | Ra (Roughness Average) | Rz (Mean Roughness Depth) |
|---|---|---|
| What it measures | Mean absolute deviation from center line | Average of peak-to-valley depths |
| Sensitivity to spikes | Low — averages them out | High — captures extremes |
| Typical use | General appearance, tactile finish | Sealing, plating, fatigue-critical parts |
| Regional preference | US and general ISO work | Legacy European DIN drawings |
As a rough rule, a well-processed casting shows Rz values about four to seven times its Ra. When a supplier quotes both, compare them against this ratio to catch inconsistent measurement.
How Ra and Rz Are Measured
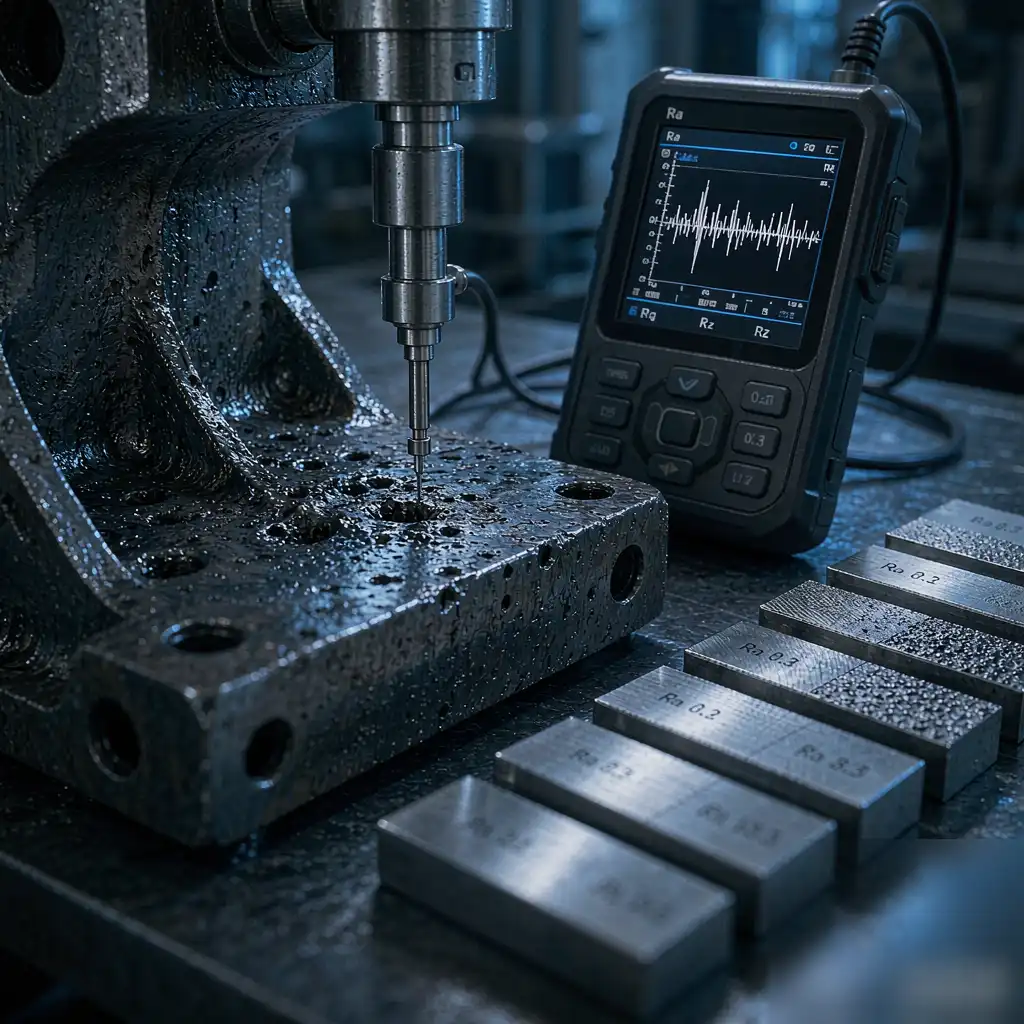
Measurement starts with a stylus tracer or optical profilometer running across the surface along a defined cutoff length. The instrument filters waviness and form, then computes the parameters from the remaining roughness profile. Because the result depends on cutoff and evaluation length, you must state those on the drawing. Otherwise, two labs will report two different numbers for the same part.
Portable meters give fast Ra checks on the shop floor, while lab profilometers deliver full Rz and 3D maps. A meter that only reads Ra cannot verify an Rz callout.
Why Rz Matters More Than You Think
Deep local valleys trap cutting fluid, plating solution, and bacteria that later bleed out in service. Consequently, a part with a beautiful Ra can still fail if its Rz is uncontrolled. For hydraulic bodies and food-contact components, this distinction is decisive.
PRACTICAL NOTE — When a seal rides on a cast face, specify Rz rather than Ra; the peak-to-valley depth governs the leak path far more than the average.
Typical Ra Targets by Application
Different functions demand different finishes. The table below lists common Ra bands for casting applications so you can benchmark your own drawings.
| Application | Typical Ra (µm) | Finishing method |
|---|---|---|
| As-cast structural (non-visible) | 6.3 – 12.5 | Shot blast only |
| Machined sealing face | 1.6 – 3.2 | CNC mill or grind |
| Hydraulic bore | 0.4 – 0.8 | Honing or lapping |
| Decorative exterior | 0.2 – 0.8 | Polish or vibratory |
These bands are starting points, not laws, and material and geometry shift them.
Surface Finish in the Casting Process Chain
Finish is set long before the finishing cell, beginning with gating, die temperature, and release agent. A casting that tears on ejection will never polish clean, no matter how much robot time you spend. Downstream grinding then removes the residual rather than fighting the root cause.
Mapping finish back to process variables lets you predict and hold spec consistently. This systems view is what separates a stable supplier from one that reworks every batch. Read our surface finishing for aluminum castings best practices to see how gating and finishing connect in practice.
The Cost of Over-Specifying Finish
Every step below the current finish costs cycle time, media, and tool wear. Dropping from Ra 1.6 to Ra 0.8 can more than double the polishing labor on a complex part. Consequently, an unnecessarily tight callout quietly inflates unit cost across the whole production run. Review each face and ask whether the function truly needs that number.
We routinely find drawings carrying decorative-grade finishes on hidden internal surfaces. Removing those saves real money without changing performance.
Achieving Consistent Finish with Robotic Finishing
Manual finishing varies with operator and shift, which makes Ra Rz hard to hold batch to batch. Robotic cells apply controlled force, speed, and path so the same program yields the same surface every time. This consistency is why automated lines win repeat contracts.
Our automated die casting deburring and grinding guide details how force-controlled robotics hit both Ra and Rz targets without over-grinding thin walls. The same cell that deburrs can feather parting lines to a specified roughness in one setup.
ROI SIGNAL — Holding finish within tolerance on the first pass typically cuts finishing labor 30–50% versus manual rework, while reducing scrap from over-grinding.
Aluminum Castings and Finish Sensitivity
Aluminum is soft and tears easily, so aggressive media quickly smears rather than cuts the surface. Therefore, aluminum needs gentler, well-tuned processes that preserve the underlying profile integrity. Specifying finish on aluminum also means controlling the prior machining marks.
Because alloy and temper change how the surface responds, validate finish on the actual production material. Our how to deburr aluminum die castings with automation covers media selection and force limits that keep aluminum finishes repeatable and clean.
Common Specifying Mistakes to Avoid
Many drawings carry errors that cost money without improving the part. Watch for these frequent issues:
- Calling out Ra on a surface that actually needs an Rz limit for sealing.
- Quoting a finish without stating cutoff length or evaluation length.
- Applying one tight value to every face regardless of function.
- Mixing DIN Rz and ISO Ra on the same drawing without conversion notes.
- Assuming a comparator swipe equals a calibrated profilometer reading.
Fixing these five habits removes most finish-related disputes with suppliers. Clear symbols beat lengthy arguments on the shop floor every time.
Choosing the Right Standard for Your Part
Start from function: does the surface seal, slide, reflect, or simply sit hidden? If it seals or carries coating, lead with Rz and use Ra as a secondary check. For tactile or visual faces, Ra alone is usually sufficient and simpler to verify.
Align your internal standard with your customer’s drawing rather than guessing at conversion. When in doubt, ask the supplier to confirm the measurement routine before the first article. That single conversation prevents the majority of finish rejects.
Bringing It Together on the Production Floor
Surface finish standards Ra Rz are not abstract symbols but practical controls on cost and performance. Treat them as a shared language between design, quality, and the finishing cell. With the right parameter on the right face, you hold spec, cut scrap, and ship consistent castings.
Measuring Roughness the Right Way
A single Ra number means little without the measurement routine behind it. State the cutoff length, the evaluation length, and the number of sampling lengths, because each changes the reported value. Therefore, agree the routine with your customer before the first article and record it in the inspection plan. Consistency in measurement matters as much as consistency in the process itself.
How Robotic Finishing Stabilizes the Numbers
Manual polishing swings with the operator and the shift, which widens the spread of both Ra and Rz. A robotic cell repeats the same force, speed, and path, so the distribution tightens and out-of-spec parts fall. This is why automated lines hold finish across long runs where manual cells drift. Stable process, stable numbers, fewer arguments about what the drawing really meant.
Documenting Finish Requirements for Suppliers
Hand your finishing partner a complete callout, not just a target value. Include the standard, the parameter, the cutoff, and the acceptance band so there is no room for interpretation. Furthermore, supply a reference part they can measure against their own profilometer. Clear documentation turns finish from a recurring dispute into a checked box on the quality plan.
Finish, Cost, and the Bottom Line
Every roughness step below necessity costs cycle time, media, and tool wear that compounds across the whole run. Conversely, an under-specified finish invites coating failure or leakage that surfaces only at the customer. The skill is matching the callout to the function and nothing tighter. When design, quality, and the cell share one clear standard, finish becomes a controlled cost instead of a recurring surprise on the monthly scrap report.
Figures are illustrative; actual results depend on part geometry, material, and cell configuration.