How to Structure an OEM Aluminum Die Casting Supply Program
Most buyers treat OEM aluminum die casting as a purchasing exercise: send a 3D model, collect three quotes, pick the lowest piece price. That works fine for a one-off bracket. It fails badly when the part runs for seven years, when the tool is worth more than a year of parts, and when a single missed shipment stops your assembly line.
A supply program is a different object than a purchase order. It is a set of documents, formulas and escalation rules that survive staff turnover on both sides and say what happens when something goes wrong. On the equipment side of this industry we see which programs run for a decade and which collapse in eighteen months. The difference is rarely the machine; it is whether the commercial and technical framework was written down before the first shot.
Program definition and the kickoff document package
The kickoff package is the most useful artifact in the whole relationship. If it is thin, every later disagreement becomes a negotiation. Below is the minimum a buyer should assemble before releasing a program for quotation. Anything missing here gets discovered later, at higher cost.
| Document | Must contain | Why it matters commercially |
|---|---|---|
| Part data package | STEP model, 2D drawing with GD&T, revision, material spec, annual volume, target price | Fixes the baseline for every later DFM change and price renegotiation |
| Engineering specification | Alloy, heat treat state, mechanical minima, critical-to-function dimensions, cosmetic class | Defines acceptance before production, not after |
| Volume profile | 12-month monthly forecast, 3-year annual estimate, peak/trough ratio, ramp curve | Drives cavity count, machine selection and capacity reservation |
| Quality requirements | PPAP level, Cpk targets, sampling plan, RoHS/REACH or IMDS declarations | Determines inspection labour and gauge investment in the price |
| Packaging and logistics | Pack configuration, pallet standard, Incoterms, ship-to region | Typically 3-8% of landed cost, most common source of surprises |
| Secondary operations | Trim, blast, CNC, tapping, leak test, impregnation, coating, assembly | Often 40-60% of delivered cost on cosmetic parts |
| Service life | Program duration, service-parts years after EOP, last-time-buy rule | Prevents a tool scrap dispute at year six |
Freeze the revision at kickoff and require written change control afterwards: a tool is cut to a specific geometry, and moving one rib can mean a new slide, a weld-back and a re-cut, at 15-30% of original tool cost. State the ramp too, because 2,000 to 40,000 pieces per month in ninety days needs a different die thermal design and a different deburring solution than growth spread over two years.
The DFM loop, and who pays for it
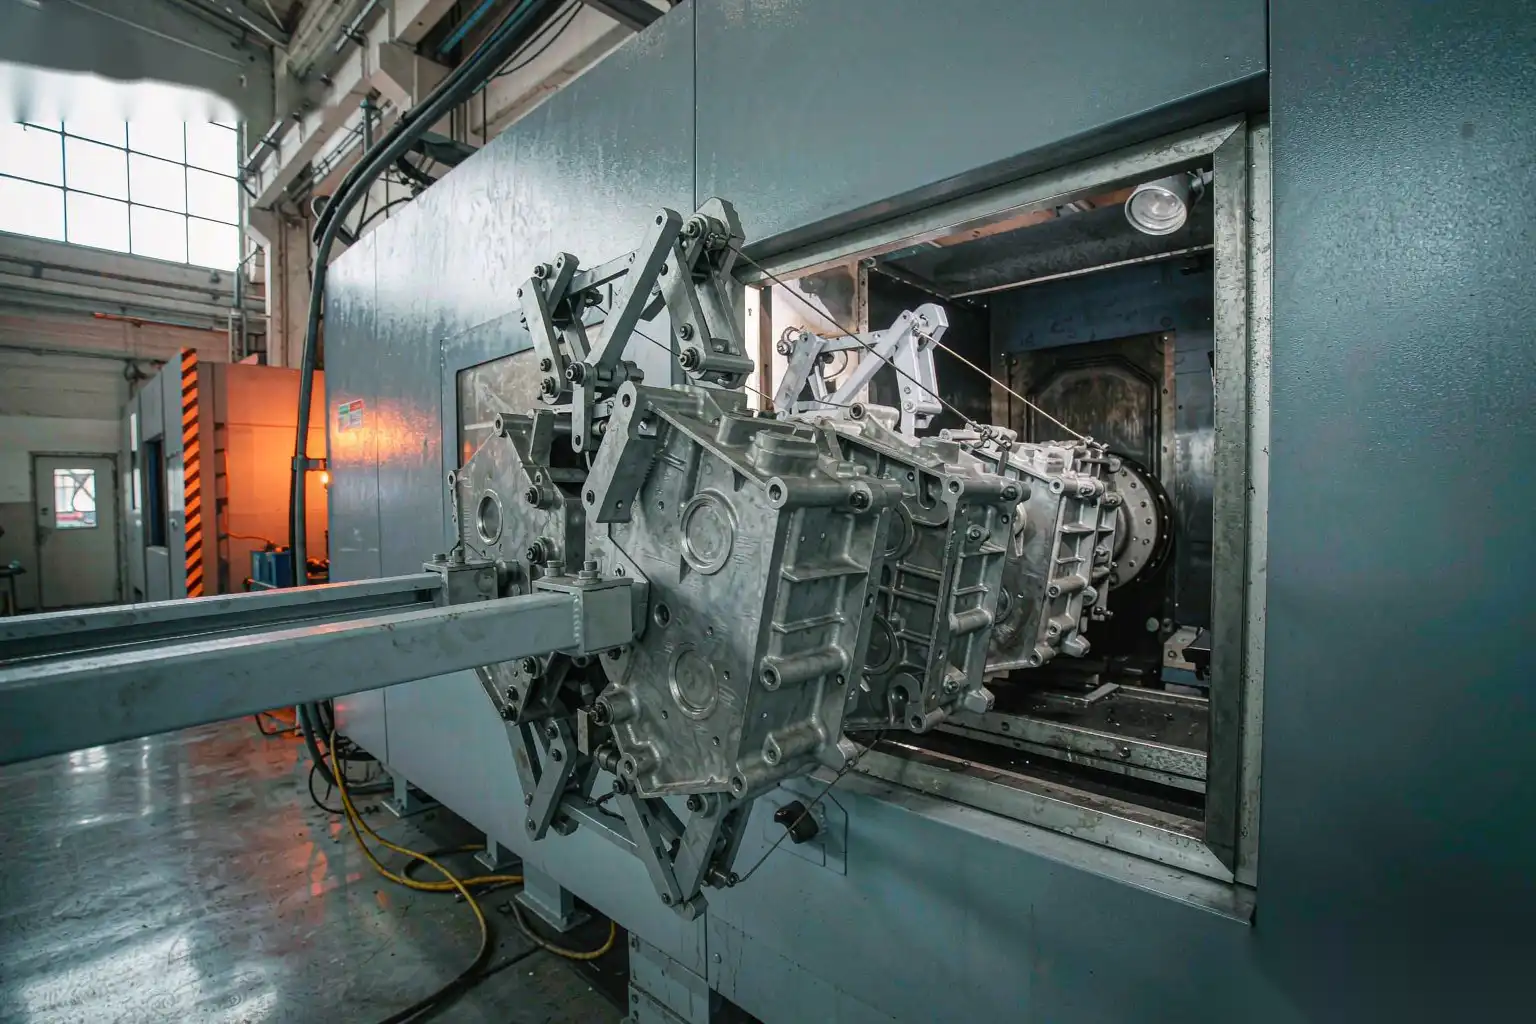
Die casting DFM is not a review meeting, it is a loop with a defined exit. Four gates:
- Gate 1, castability review (3-5 days). Wall distribution, minimum wall at the projected area, draft, radii, coring feasibility, parting line, ejection balance.
- Gate 2, tooling concept (5-10 days). Cavity layout, gating and overflow scheme, runner balance, cooling layout, slide and lifter count, shot weight.
- Gate 3, simulation (3-7 days). Fill, solidification, predicted porosity location, die thermal balance at steady state, cycle time.
- Gate 4, freeze and release. Buyer signs the geometry; the tool is cut to the signed revision.
The economics buyers get wrong: the loop is only valuable if it changes the design. Make the supplier quantify each recommendation, for example draft on a 60 mm deep pocket raised from 0.5° to 1.5° to cut drag-mark scrap, or a 3 mm wall replaced by 2.5 mm plus a rib to shorten fill time and reduce gas porosity at the last-fill point. A clean report with no findings means either an easy part or no real review.
Above roughly 100,000 pieces per year, engineering is normally absorbed into tooling; below that, expect a fee or a higher tooling price. Avoid unpaid DFM, because unpaid work gets done last.
Tooling ownership, amortization and life clauses
This clause decides more money than the piece price does. Write down all five points below.
- Ownership. The tool is yours even though it sits in their plant. Say so, with the right to move it on written notice after a defined notice period and settlement of any unpaid balance.
- Title marking. Engraved plates with your part number, asset number and build year, photographed into the contract appendix.
- Amortization vs lump sum. Amortized tooling lowers upfront cash but creates lock-in: the piece price carries a per-part recovery, and moving the tool becomes a buyout. Typical structures are 100% prepaid, 50/50, or amortization over 30-50% of quoted tool life.
- Tool life commitment. State it in shots, not years. For cold chamber aluminum in nitrided H13 or equivalent, expect 80,000-150,000 shots for a moderately complex tool and 150,000-300,000 for a simple one on A380-class alloys. Ask what is included: re-nitriding, slide inserts, core pins.
- Maintenance, dormancy and storage. Who pays routine maintenance, what happens after twelve months with no orders, and who authorizes scrapping. Require return of the tool in a defined condition with a current wear-parts list; a tool without its core pin set is effectively scrap. Our aluminum die casting tooling guide covers the maintenance intervals.
Volume commitments and capacity reservation
Volume clauses cut both ways. Miss a committed number and you owe something; commit nothing and you get scheduled last when capacity is tight.
- Rolling 90-day firm quantity, plus a 9-month rolling forecast that carries no liability but drives material and tool maintenance planning.
- A tolerance band on the firm window, typically ±15%. Inside it, price and delivery hold; outside it, lead time may be re-quoted and expediting cost added above the band.
- Capacity named explicitly: the machine tonnage and the shifts the program is booked against. A 250-800 tonne machine on two shifts gives roughly 900-1,100 productive hours per month per shift.
- Last-time-buy and service-parts terms at kickoff, typically 5-10 years after end of production, with a minimum annual quantity or a storage fee.
Do the last-time-buy math: if service demand is 400 pieces per year and the economic lot is 2,000 shots, you buy five years of inventory in one run. Price that storage, and check whether the alloy and any plating have a shelf life.
Price adjustment formula tied to the aluminum ingot index
Aluminum is roughly 40-60% of the raw material line and the ingot price moves enough to matter. A fixed three-year price is a bet, and the supplier prices the risk into it; an index-linked clause is cheaper for both sides. A workable formula:
P = P0 + W × (M1 − M0) / 1000 × K
Where P0 is the base piece price at signature, M0 the reference ingot index at signature in USD per tonne from a named public source, M1 the index at the adjustment date, W the net casting weight in kilograms, and K the yield factor, typically 1.10-1.25, covering runner, biscuit, overflows, melt loss and trim scrap recovery.
Mechanics to specify:
| Parameter | Recommended setting | Note |
|---|---|---|
| Review frequency | Quarterly, first working day | Monthly is too noisy; annual exposes you to large jumps |
| Trigger band | No change if index moves under ±5% | Avoids administrative churn |
| Cap and floor | ±15% cumulative per review cycle | Beyond this, reopen the whole price |
| Index source | Named public settlement price | Never a supplier-internal number |
| Scrap credit | Gate-return value at a published secondary alloy discount | Worth a few percent of the material line |
| Non-metal inputs | Energy, die steel and labour adjusted annually | Keeps the quarterly clause to metal only |
Worked example: 1.4 kg net casting, yield factor 1.18, base index USD 2,200/t, index moves to USD 2,480/t. Delta 280/t; 1.4 × 1.18 = 1.652 kg; adjustment = 280 × 1.652 / 1000 = USD 0.46 per piece. On 40,000 pieces a year that is USD 18,500, which is not a rounding error. Also state what the clause does not cover: FX, drawing changes, specification changes and volume changes all sit outside the metal adjustment.
Quality agreement and acceptance criteria
The quality agreement is the document that ends arguments. Write it before PPAP, and specify the measurement method, not just the tolerance.
- Critical-to-function characteristics marked on the drawing with target Cpk: ≥ 1.33 on machined and assembly-critical dimensions, ≥ 1.00 on as-cast dimensions, ≥ 1.67 where the dimension is safety related or feeds a sealing face.
- Measurement method per characteristic: CMM, functional gauge, vision, air gauge or manual. Measured two ways, one dimension gives two Cpk values.
- Sampling: full first-piece layout on every setup, then in-process checks, commonly one piece per shift per cavity minimum, escalating to five per hour on a drifting characteristic.
- Porosity acceptance: name the standard and the reference radiograph level, and define the inspection zone. Gate areas and heavy sections are not sealing faces.
- Leak test: method, test pressure, limit in cm³/min or Pa/s, on 100% of parts or at a stated AQL.
- Cosmetics: a referenced surface standard plus physical limit samples signed by both parties and replaced on a defined cycle.
- Nonconformance: containment in 24 hours, root cause in 5 working days, permanent corrective action in 20 working days, in 8D format.
- Record retention: 10 years for automotive, 3-5 years otherwise.
One clause saves the most money: the supplier may not change process parameters, alloy source, release agent or sub-supplier without written notice. Uncontrolled parameter drift is the root cause of most “fine for two years, now it leaks” cases. The full sequence from incoming alloy to PPAP sign-off is set out in our custom aluminum die casting guide.
Single-source versus dual-source
Dual sourcing is real risk reduction, but it carries costs that belong in the decision.
Costs of dual sourcing:
- Two tooling sets, typically 1.3-1.6× the per-tool cost once geometry matching and a second gauge set are included.
- Two PPAP packages, two sets of limit samples, two audits.
- Split volume raises price on both halves: a 60/40 split of 100,000 pieces costs more per piece on each side than a single-source 100,000 award, typically 4-9%.
- Divergent process windows mean the two suppliers’ as-cast dimensions differ, which matters if machining fixtures are shared.
The benefits are supply continuity against fire, labour action, curtailment or capacity failure; commercial tension at annual reviews; and a validated fall-back when you must ramp faster than one plant can absorb.
Our recommendation: single-source tooling and casting for the first 12-18 months while the process stabilizes, then decide. Splitting a part whose process window is not yet understood doubles the debugging effort. Once stable, if the program exceeds roughly 250,000 pieces per year or feeds a single-plant assembly, qualify a second source and hold it on 5-10% annual volume so the tooling does not go cold. Go dual source from day one only for safety parts, parts with long lead-time coatings, or programs in regions with volatile power supply.
IP protection, exclusivity and the escalation path
IP protection. The realistic risks are not the drawing file being stolen. They are the tool being run for someone else, the design shown to a competitor as a capability example, and process know-how leaving with a technician. Controls that work: an NDA running 5-10 years past program end covering drawings, tooling design and process parameters; a no-use clause barring production, sampling or exhibition for any other party; a no-photography clause over the cell with a named CAD access list; ownership of buyer-funded process parameters; segregated access-controlled tool storage; and a named jurisdiction and enforcement forum, because an NDA without a venue is close to decorative in cross-border programs.
Exclusivity. Buyer-side exclusivity is usually free, since the tool is yours anyway. Supplier-side exclusivity should be paid for visibly, through a lower piece price, a tooling credit or a capacity guarantee. If you grant it, cap it in time and tie it to performance: it ends automatically after two consecutive quarterly delivery ratings below the agreed threshold.
Escalation path. Write the ladder with names, roles, response times and a deadlock step.
| Level | Trigger | Participants | Response |
|---|---|---|---|
| 1 | Lot nonconformance, slip under 5 days | Supplier supervisor + buyer SQE | 24 h, containment |
| 2 | Repeat nonconformance, line stoppage, slip over 5 days | Supplier plant manager + buyer supply chain manager | 72 h, recovery plan |
| 3 | Line-down, safety issue, chronic failure over 2 months | Supplier GM + buyer operations director | Same day, plan in 5 days |
| 4 | Unresolved after 30 days at Level 3 | Executive sponsors | 10 days |
| 5 | Deadlock | Named mediation or arbitration venue | Per contract |
Add the tool release clause: if Level 4 fails, you have the right to move the tool and drawings to an alternative supplier, with the incumbent obligated to cooperate within a defined number of days at defined hourly rates. Without that, escalation is theatre.
Where the finishing cells fit in the program
On most OEM programs the casting is only half the cost. Trimming, CNC, deburring, grinding and polishing routinely represent 40-60% of delivered cost on a cosmetic part, and they set your capacity ceiling rather than machine tonnage. Size the finishing cell at the same time you size the die casting machine: a cell that deburrs 90 pieces per hour will not support a 120 per hour casting rate.
This is the part of the program we work on. DZ Machinery builds 6-axis robotic deburring and grinding cells with force-controlled floating spindles, pneumatic or compliant belt heads, automatic tool change and multi-station rotary tables, plus polishing cells with belt, cloth and sisal stations and automatic compound feed. We also integrate the line around the cell, from core shooting and low-pressure or gravity casting through band sawing of the runner, CNC, robotic grinding, automatic polishing and inspection, together with fixtures, dust extraction and guarding.
Bring us two things early. First, part geometry and the burr specification: 0.2 mm of allowance on a parting line is a belt operation, while 3 mm of flash on a slider witness mark is a spindle and carbide burr operation, and the cycle times differ by a factor of three or more. Second, your ramp curve, because a cell sized for year-three volume and run at 30% utilization in year one has a different payback than a modular cell that grows with the program.
If you are laying out finishing stages now, our engineering team can review your part drawings and return a cycle time and station count estimate before you commit the rest of the line. For the finishing route options themselves, aluminum die casting finishing options is a useful companion to the commercial structure above.