Hydraulic Fitting Grinding: Precision for High-Pressure Parts
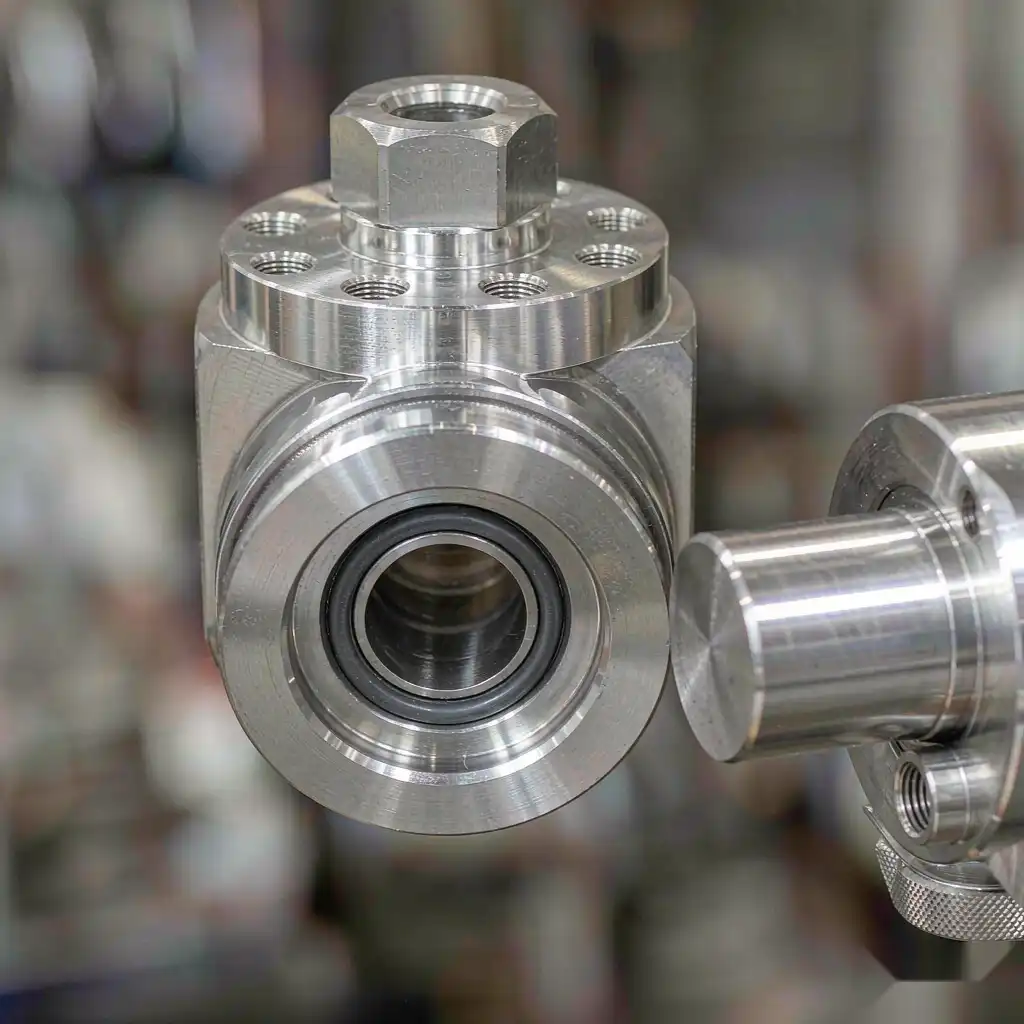
A hydraulics shop in northern Italy was rejecting fittings at the pressure test because the seats were not round — a hand ground seat varied a few microns part to part, and at 350 bar that few microns leaked. “The print says round,” the engineer said, “and the hand says close enough.” Hydraulic fitting grinding is a roundness job: the seat has to be precise because the seal lives or dies on it.
This guide covers how to grind hydraulic fittings to the roundness high-pressure service needs.
Why Roundness Is the Whole Job
A hydraulic seal presses on a seat. If the seat is not round, the seal touches in spots, the load concentrates, and it weeps or blows. Hand grinding drifts with the operator and the hour. The seat has to be round and repeatable, not just shiny.
How Robotic Grinding Holds Roundness
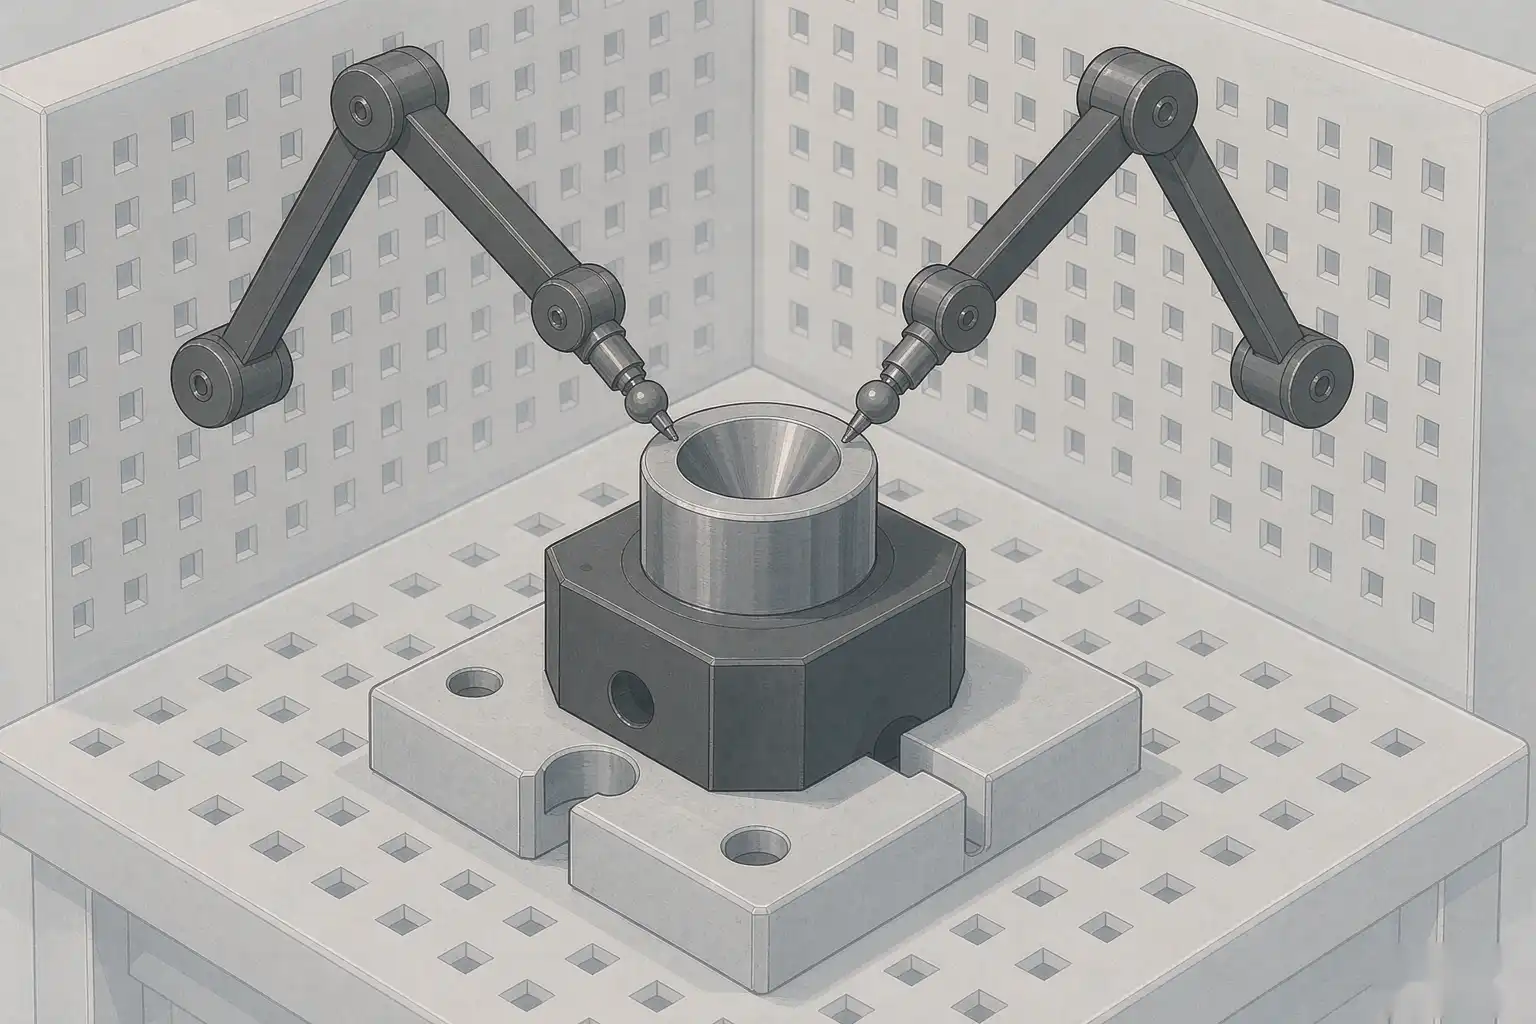
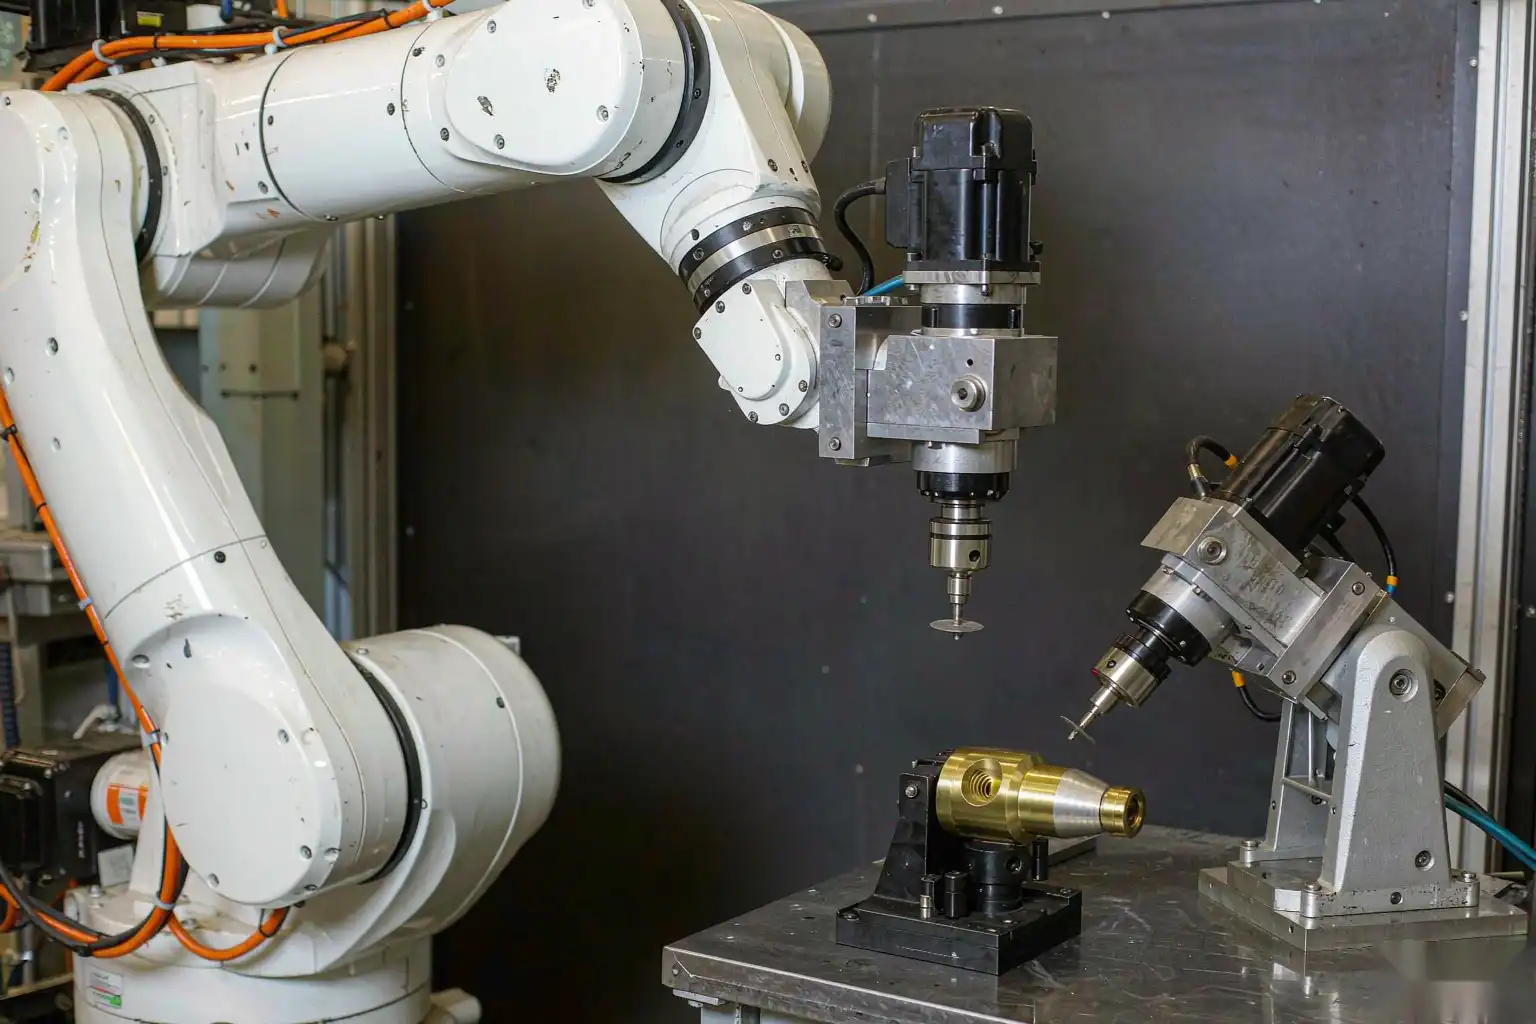
A robotic cell locates the fitting on a fixed datum and grinds the seat at locked force, following the true axis every cycle. Force control is what keeps the seat round instead of egg-shaped under hand pressure. Every fitting leaves matched, which is what a pressure test demands. The round-seat logic is the same one we use on ball valve grinding for a leak-free seal.
For high-pressure bodies in general, the same precision discipline shows up in pipe fitting deburring before the seat is cut.
What Has to Be True First
Fixed Datum
Locate the fitting on its true center so the robot grinds the seat concentric. A shifted datum finishes one side harder than the other and the seat goes egg-shaped.
True Axis Path
The wheel must track the bore axis, not the casting’s outer drift. Program to the seat, not the blank.
Measured Roundness
Roundness is not visible. Measure it on the way out so the cell holds the spec across the run, not just on the first part.
Three Mistakes Buyers Make
1. Grinding inconsistent blanks. Automation exposes a drifting seat. Fix the casting first.
2. Skipping force control. Fixed-path without force feedback leaves the seat egg-shaped. Force control holds it round.
3. Not measuring roundness. A shiny seat can still leak. Measure on the way out so the spec holds.
Frequently Asked Questions
Can a robot hold roundness better than a hand grinder?
It holds it across the run. A hand finisher peaks on one seat; a cell matches every seat, which is what a pressure test judges.
Which fittings suit automated grinding?
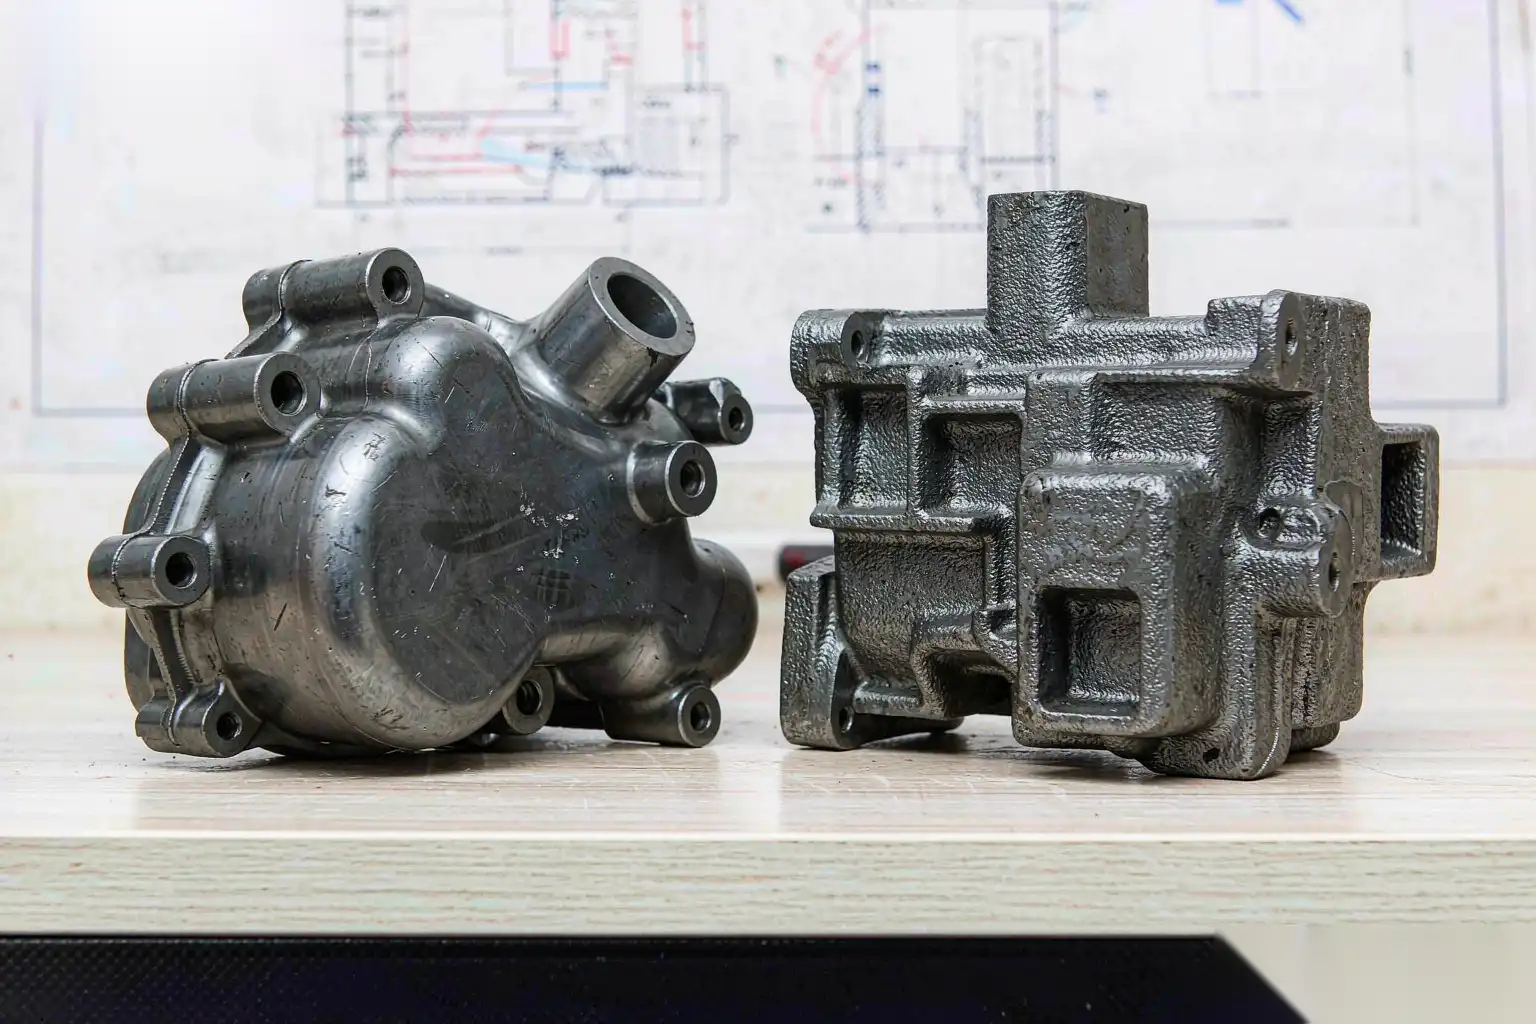
Seated fittings, adapters, and manifolds with a round seal face. Mixed sizes run with quick-change fixtures and stored programs.
How many fittings fit one cell?
Several, with quick-change fixtures. Design changeover in so mixed-SKU runs do not stall the cell.
This guide was prepared by the application engineering team at Xiamen Dingzhu Intelligent Equipment Co., Ltd. (DZ Machinery), which designs and commissions deburring, grinding, polishing, and die-casting lines for manufacturers across more than a dozen countries. Finish notes reflect typical hydraulic fitting outcomes; confirm against your alloy and pressure spec before purchase.
Tags: High Precision Hydraulic Casting Finishing, grinding, Robotic Grinding, surface finish, surface quality, plumbing fittings