


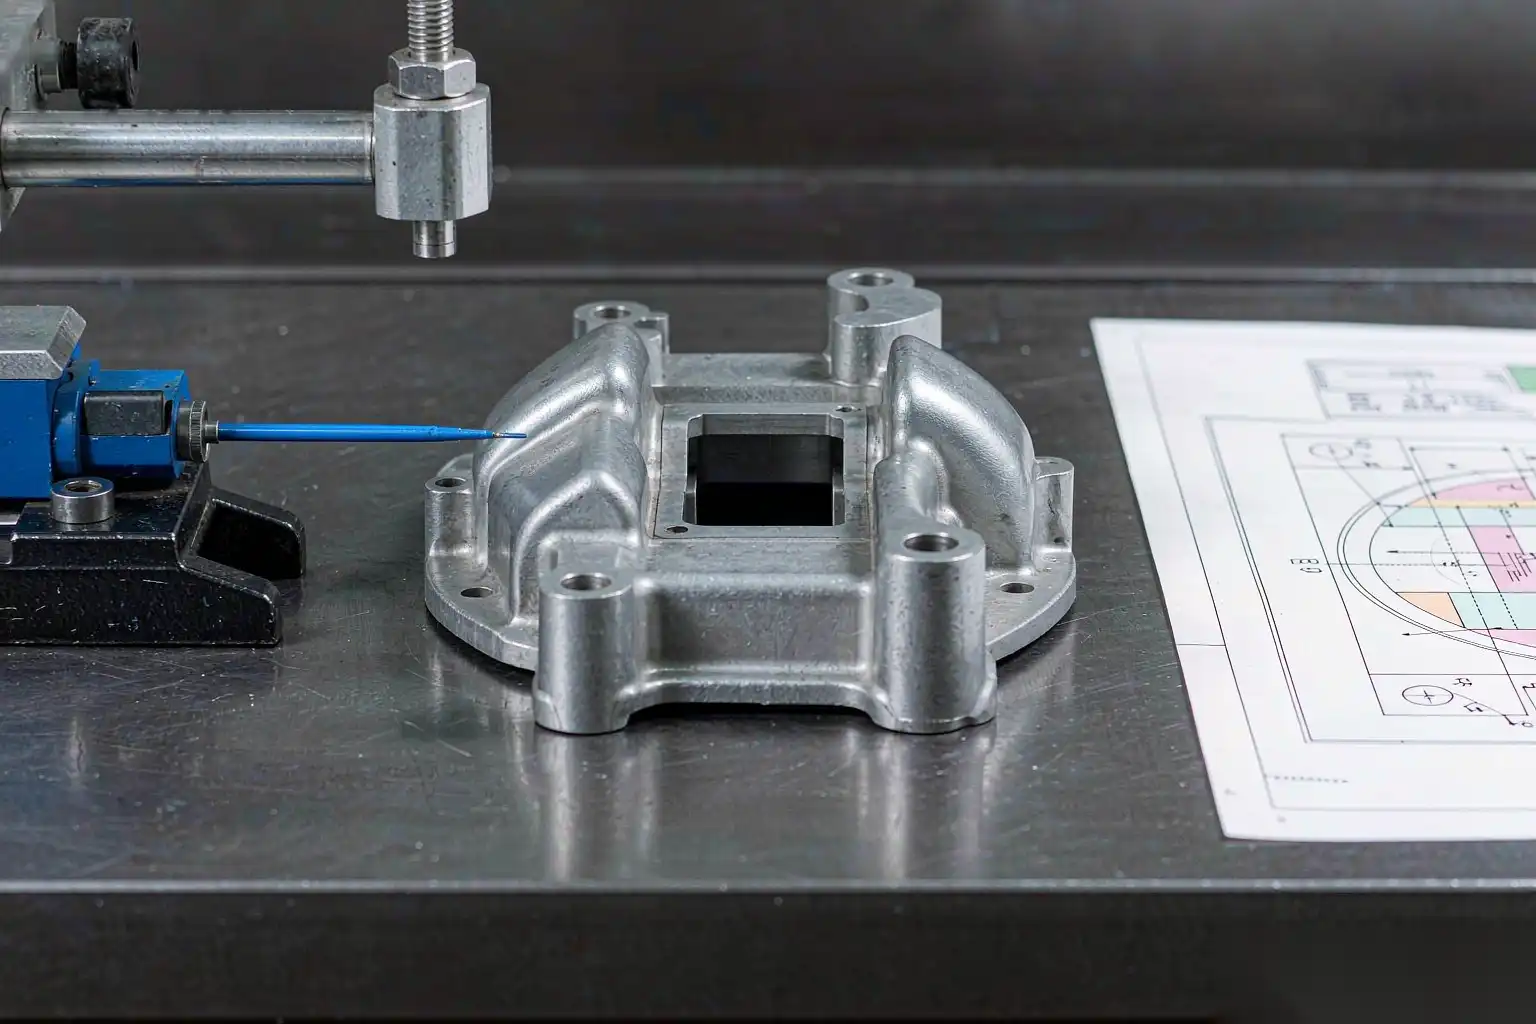
First Article Inspection for Aluminum Die Castings: A Practitioner’s Checklist
First article inspection is where a die casting program either earns confidence or loses three weeks. Done properly, it proves that a new tool, a new machine setting and a new process window produce parts that meet every drawing requirement. Done casually, it produces a stack of numbers nobody trusts and a second sampling round that delays shipment. This guide is the version I wish every supplier ran before sending us a report.
What FAI Is Actually For
First article inspection answers four questions, in this order:
- Does this part meet every drawing requirement, measured on parts made from production tooling under production conditions?
- Is the measurement itself credible — correct equipment, calibrated, correct datum setup, correct sample size?
- Is the process capable of repeating this result, or did we just get three lucky parts?
- Is the documentation adequate for the customer’s quality system and for traceability two years from now?
Note the emphasis on production conditions. A part made at reduced speed, with extra trimming passes and hand-selected material, teaches you nothing. Insist that FAI parts come from a normal production run at nominal parameters.
Preparing Before the First Part Arrives

Most FAI failures are preparation failures. Three documents must exist before parts.
- A ballooned drawing. Every characteristic gets a numbered balloon. This is the index that ties measurements to features and prevents the classic argument about which dimension you actually checked.
- An identified datum structure. The drawing must establish primary, secondary and tertiary datums. If it does not, resolve it before sampling — not during measurement. Casting datum selection has its own logic, covered in detail in our aluminum die casting tolerances guide.
- A control plan draft. Even a rough one. It lists each key characteristic, the measurement method, the sample frequency and the reaction plan.
You also need the material certificates (alloy chemistry and heat identity), the heat treatment record if applicable, and the parameter sheet from the casting cell. Without these, a dimensional pass is meaningless because you cannot reproduce it.
Sample Size: More Than Three
The default in many shops is three pieces. That is the minimum for a layout report, not a sufficient basis for process confidence.
| Purpose | Recommended sample | Notes |
|---|---|---|
| Full dimensional layout | 3 pieces | Minimum to demonstrate the tool makes nominal geometry |
| Key characteristic capability | 30 pieces | Supports a Ppk calculation with statistical meaning |
| Destructive and porosity checks | 3 to 5 pieces | Cut-up, X-ray or CT, cross-section, leak test |
| Cosmetic and finish approval | 3 pieces plus limit samples | Requires agreed boundary samples, not adjectives |
If your customer requires a capability study, plan for 30 pieces from one production run, ideally consecutive. If they only require a layout, three pieces plus a documented process window is acceptable — but say so explicitly in the report so nobody assumes more.
Layout Versus Functional Gauging
CMM is not always the right answer, and using it everywhere wastes time.
Use CMM when:
- GD and T callouts require true position, profile of a surface, or perpendicularity to a datum
- You need actual values for trend analysis and process adjustment
- The part is complex enough that functional gauges would be expensive to build
Use functional gauges when:
- The feature’s function is assembly fit, and a go/no-go attribute check mirrors reality
- You need rapid checking at the machine rather than in a metrology lab
- The tolerance is tight and CMM measurement uncertainty approaches the tolerance band
Watch measurement uncertainty. A callout of ±0.025 mm should not be verified with equipment whose uncertainty is ±0.015 mm. The standard rule of thumb is that your measurement system should be capable of resolving at least one tenth of the tolerance band, which for a 0.05 mm band means equipment resolution around 0.005 mm.
Porosity Verification and Acceptance
Dimensional correctness says nothing about internal soundness. Porosity acceptance must be specified, measured and reported.
- Visual and section check. Cheapest, adequate for non-critical parts. Circle comparison charts standardise judgement.
- X-ray (film or digital). Standard approach. Specify the acceptance level explicitly, for example “no gas porosity exceeding ASTM E505 Level 2 in the sealing area”, rather than “no significant porosity”.
- CT scanning. Best for structural parts and for locating porosity relative to machined surfaces. Slower and more expensive, but it tells you where the voids are, not just that they exist.
- Leak testing. For pressure boundary parts this is usually the functional test that matters more than any image. Specify medium (air or helium), pressure, dwell time and maximum leak rate in consistent units.
If you need a refresher on how porosity forms and what actually suppresses it, our article on aluminum die casting porosity causes and solutions covers the process side in detail — useful when your FAI fails for the second time and you need root cause rather than better sorting.
A common failure mode: a part passes FAI dimensionally and then leaks in service because porosity intersected a machined sealing face. Require X-ray or CT of critical zones before machining is finalised, not after.
GD and T Evaluation of Key Characteristics
Forget measuring everything to the same standard. Classify characteristics.
- Critical characteristics. Affect safety, regulation, or function. Require capability study and 100 percent or statistically justified inspection going forward.
- Significant characteristics. Affect assembly or performance but not safety. Capability study desirable.
- Minor characteristics. Appearance and non-functional geometry. Attribute inspection sufficient.
For each true position callout, confirm you have evaluated it in the correct datum reference frame and with correct material condition modifiers. Maximum material condition (MMC) gives bonus tolerance, and ignoring it causes false rejects. Conversely, treating everything as regardless of feature size when the drawing says otherwise causes false accepts.
Report actual measured values, not pass/fail verdicts. A value near the tolerance limit is a warning even when technically compliant.
Documentation Levels and What Buyers Ask For
Expectations differ by industry. A sensible middle ground most suppliers can meet:
- Level 3 style submission. Completed layout forms, ballooned drawing with all balloons addressed, material certificates, porosity results, cosmetic approval, a process flow and a preliminary control plan.
- Level 4 style submission. Everything above plus capability data on critical characteristics, process failure mode analysis, measurement system analysis, and gage repeatability evidence.
At minimum, the report package should contain:
- Cover sheet with part number, revision, date and the exact production conditions used
- Ballooned drawing with every balloon accounted for
- Measured values table with tolerance, actual, deviation and verdict per characteristic
- Material and heat treatment certificates traceable to melt and batch
- Porosity and/or leak test results with acceptance criteria stated
- Signed approval by the responsible quality engineer
Note the part revision level. FAI against the wrong revision invalidates the whole exercise, and it happens more often than anyone admits.
Linking FAI to Ongoing Control
FAI is not a one time event; it is the baseline for subsequent control.
- Transfer the critical characteristics from the layout into the production control plan with defined sample sizes and frequencies.
- Keep the FAI parts as physical limits. Mark them, store them, and use them when a specification argument arises nine months later.
- Re-run relevant portions after any tool repair, insert change, parameter change beyond the validated window, or supplier change of alloy lot source. Document the trigger rules so it is not a judgement call each time.
Common Mistakes That Force a Repeat Round
These account for most rejections I see:
- Samples produced under special conditions rather than normal production parameters
- Missing balloons, or a ballooned drawing that does not match the drawing revision
- No porosity or leak test results despite the part being a pressure boundary
- Only three pieces submitted when a capability study was requested
- Measurement reports without actual values, only pass/fail
- No material certificates, or certificates that do not trace to the part lot
- Datum setup inconsistent with the drawing datum structure
- Cosmetic criteria described in words rather than agreed limit samples
Each of these costs two to three weeks of calendar time. All of them are avoidable in an afternoon of preparation.
A Practical Buyer Checklist
Before you approve an FAI submission, verify:
- Part revision matches your current drawing revision
- Samples came from production tooling at production parameters
- Every balloon has a measured value, not just a verdict
- Critical characteristics have capability data if you required it
- Porosity and leak results specify the acceptance criteria used
- Material and heat treatment certificates are present and traceable
- The control plan lists the same key characteristics you care about
- Physical approved samples are retained and labelled on both sides of the relationship
How Long FAI Should Take, and Why It Slips
Timeline realism helps both sides. A competent supplier with prepared documentation can complete a dimensional layout in two to four working days once parts exist. Adding porosity examination typically adds three to five days, because sectioning, mounting, polishing and evaluation are sequential operations that cannot be compressed by enthusiasm. If heat treatment is involved, specimen conditioning for representative properties adds further calendar time.
Programmes slip for predictable reasons. Tooling adjustments mean resampling. Disagreement over datum structure means remeasurement. Missing material certificates stop the package dead. Awaiting customer clarification on an ambiguous callout can add a week.
You can compress most of this with two habits. First, agree the datum scheme and the key characteristic list at quotation stage, before any steel is cut — these decisions cost an hour early and several weeks late. Second, require the supplier to send the ballooned drawing for approval before they start measuring. Catching a wrongly identified key characteristic on the drawing costs nothing; catching it in the report means another full layout.
Finally, treat turnaround time as a supplier qualification signal. A supplier who consistently needs three rounds to produce a usable first article package will predictably struggle with production control later, because the underlying cause is usually documentation discipline rather than metrology capability. If you want a second opinion on a first article package before you sign it off, send it to our engineering team and we will walk through it with you.



