Mass Finishing Machine: Complete Guide for Metal Shops
If your shop finishes metal parts one at a time, you are paying for every edge twice — once to make it and once to deburr it by hand. A mass finishing machine changes that arithmetic. Instead of an operator working a file or a buff across a single component, the entire batch is finished at once as abrasive media rubs against every exposed surface inside a vibrating or rotating chamber. For die-castings, stampings, forgings, and machined hardware, it is the fastest route from rough part to repeatable, plate-ready surface. This guide explains how mass finishing works, the machine types worth comparing, how to pick media, and how to size a system to your real throughput.
What Is a Mass Finishing Machine?
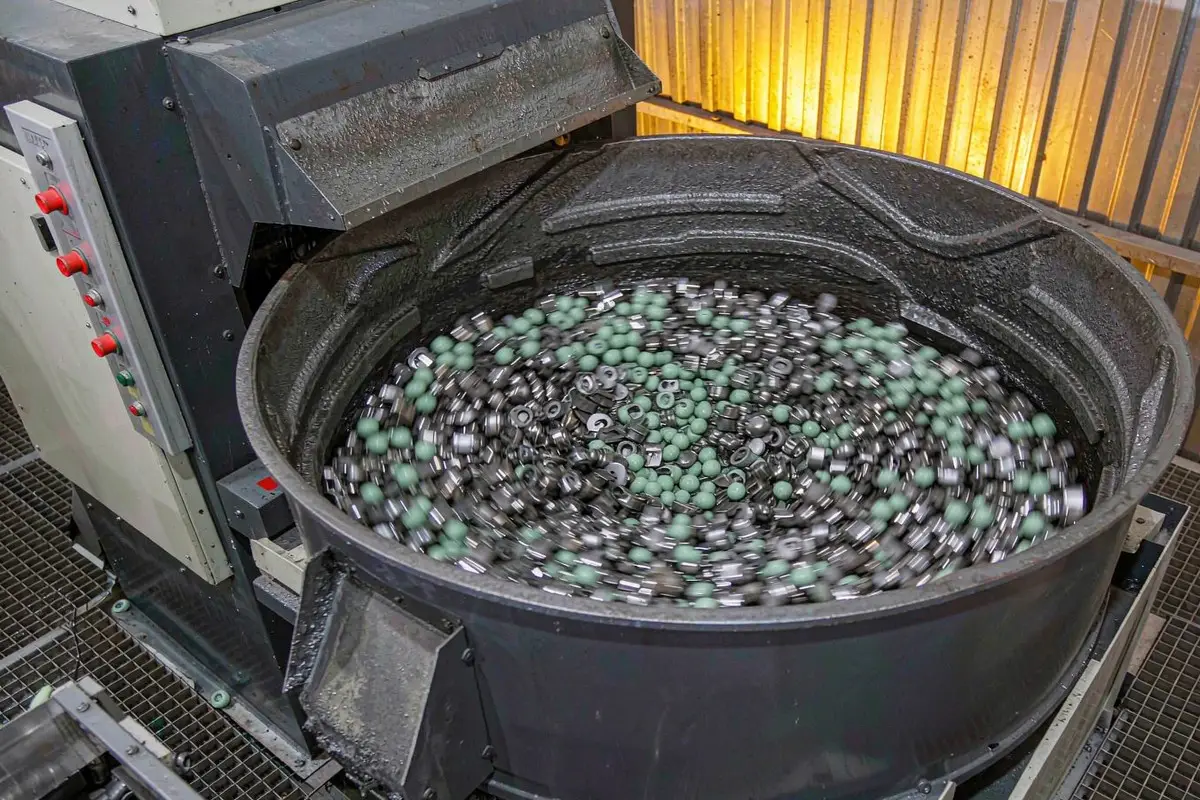
A mass finishing machine is a batch surface-treatment system that deburrs, descales, radiates edges, cleans, and polishes large quantities of parts simultaneously. The parts are loaded into a chamber together with abrasive media, water, and a liquid compound. Mechanical energy — vibration, rotation, centrifugal force, or drag motion — keeps the media and parts in constant, controlled contact, so thousands of microscopic abrasive actions happen every minute.
The defining advantage is uniformity. Because every part in the load sees broadly the same media action, edge radii and surface roughness come out consistent from the first piece to the last. That consistency is what hand finishing cannot deliver at volume, and it is why mass finishing sits at the front of most modern finishing lines, ahead of plating, coating, or precision polishing.
How Does Mass Finishing Work?
The physics differ by machine type, but the process logic is the same across the category:
- Load the chamber. Parts, media, water, and compound go in together. The media-to-part ratio is the single most important setup variable.
- Apply mechanical energy. An eccentric-weight motor, a rotating barrel, a spinning disc, or a drag spindle forces the mass into continuous relative motion.
- Create rolling contact. The media bed lifts, tumbles, and folds, so abrasive surfaces repeatedly strike and slide across part edges and faces.
- Cut or burnish. Coarse media removes burrs and stock aggressively; fine media and steel media smooth and brighten the surface.
- Separate, rinse, and dry. Parts are screened or magnetically separated from media, then rinsed and dried before the next operation.
Cycle times range from about 15–30 minutes for light deburring to several hours for heavy stock removal or a bright cosmetic finish. Compound chemistry — pH, lubricity, and surfactant package — controls how clean the media stays and whether parts rust between batches.
Mass Finishing Machine Types Compared
Four configurations cover most production needs. The right choice depends on part geometry, batch size, and the finish target:
| Machine Type | Motion | Typical Cycle | Best For |
|---|---|---|---|
| Vibratory bowl | Toroidal vibration | 20 min – 3 h | Small-to-medium parts, bulk deburring and radiusing |
| Vibratory tub | Linear trough vibration | 20 min – 4 h | Long, large, or fixtured components |
| Centrifugal disc | High-energy disc rotation | 3 – 20 min | Small robust parts needing fast fine finish |
| Drag finisher | Fixtured spindle through media | 5 – 30 min | High-value, delicate, or complex parts |
Vibratory bowls and tubs are the workhorses and are covered in depth in our vibratory finishing machine buyer’s guide. Centrifugal disc machines trade gentle handling for speed, while drag finishers protect parts that cannot touch each other.
Choosing the Right Mass Finishing Media
Media is the cutting tool of the process. Match its material, shape, and size to your alloy and finish target:
- Ceramic media — dense and long-wearing, the default for aggressive deburring on steel and hard alloys; available as cylinders, triangles, and tri-stars.
- Plastic media — lighter and gentler, ideal for aluminium, brass, and zinc die-castings where surface damage is unacceptable.
- Steel media — used for burnishing and bright, high-lustre finishes; extremely durable and non-cutting.
- Organic media — walnut shell and corn cob for drying, light polishing, and delicate work.
Shape matters as much as material: triangles and tri-stars reach into crevices and slots, while balls and cones give a smoother, more uniform action on open surfaces. Our detailed vibratory deburring media selection guide walks through size grading and media-to-part ratios.
Mass Finishing vs Other Deburring Methods
Buyers often ask how mass finishing compares with hand work and with robotic deburring. The honest answer is that they solve different problems:
| Method | Throughput | Consistency | Best Fit |
|---|---|---|---|
| Hand deburring | Low | Operator-dependent | One-off parts, rework |
| Mass finishing | Very high | High across the batch | Bulk deburring, radiusing, pre-plate prep |
| Robotic deburring | Medium | Very high per part | Complex geometry, tight tolerances |
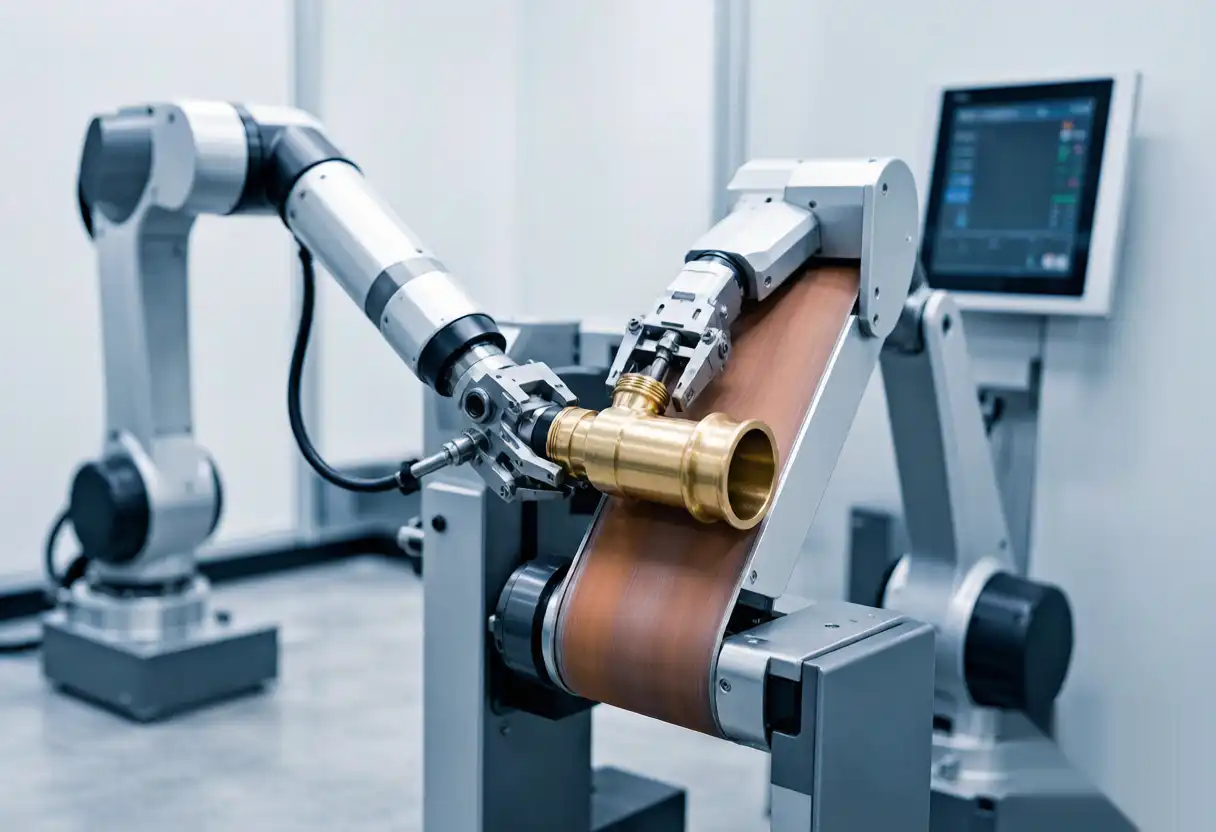
In practice the two are complementary. Mass finishing removes the bulk of the burr cheaply, then a robotic cell handles selective edges and cosmetic surfaces. That is exactly the architecture described in our end-to-end surface finishing workflow.
Key Applications Across Industries
Because mass finishing is a batch process, it pays off wherever you have volume:
- Die casting. Removes parting-line flash and gate burrs from aluminium and zinc components before machining or coating.
- Automotive. Fasteners, brackets, and housings get uniform radii that improve fatigue life and assembly fit.
- Aerospace. Precision deburring of machined parts where stress risers are unacceptable.
- Sanitary ware and hardware. Faucets, locks, and door handles are pre-finished before final polishing.
- Medical and instrument. Consistent surface preparation where process validation is required.
Benefits: Cost, Consistency, and Throughput
The business case is simple arithmetic. One mass finishing machine replaces many hours of manual filing and buffing per shift, and it does so with far less variability:
- Consistency — every part sees the same media action, which sharply reduces reject rates versus hand work.
- Lower labour cost — one operator can run several machines and a single load replaces dozens of manual operations.
- Higher throughput — batch processing shortens lead times and frees skilled labour for value-added work.
- Better durability — controlled edge radiusing removes stress concentrations that cause cracking in service.
How to Select the Right Mass Finishing Machine
Work through this checklist before you request a quotation:
- Part size and geometry. Small parts suit bowls; long parts suit tubs; tiny high-value parts suit drag or disc machines.
- Material. Hard steel needs ceramic media and higher energy; soft alloys need plastic media and lower amplitude.
- Finish target. Deburr only, radius, or bright polish — each changes media, compound, and cycle time.
- Volume and batch size. Batch or continuous? Continuous systems cost more but pay off at scale.
- Downstream steps. Plan separation, rinsing, drying, and hand-off to polishing or plating.
- Utilities and footprint. Confirm floor space, water supply, drainage, and power before delivery.
Always ask for a sample run on your actual parts. A reputable supplier will process a trial batch and size the machine to the real cycle time rather than a catalogue estimate.
Integrating Mass Finishing Into an Automated Line
Standalone machines deliver value, but the larger gain comes from connecting stages. A typical layout runs casting or stamping, then mass finishing for bulk prep, then selective robotic work, then inspection and packing. When mass finishing feeds a automatic deburring machine or a robotic polishing cell, handling drops, cycle time falls, and quality becomes repeatable. If surface texture must be controlled before coating, pairing mass finishing with a shot blasting machine gives a uniform anchor profile.
Maintenance Tips for Maximum Uptime
Mass finishing equipment is forgiving, but it rewards routine care. Inspect eccentric weights and motor mounts for looseness, monitor liner wear, refresh media and compound before glazing sets in, and keep separation screens clear. Compound concentration and pH should be checked daily, because degraded compound is the most common cause of poor cut rate and rust spotting.
Common Mistakes to Avoid
Most mass finishing problems are self-inflicted at setup:
- Overloading the chamber. Too many parts starve the media of room to circulate, producing patchy results.
- Wrong media for the alloy. Ceramic media on soft zinc die-castings gouges the surface; plastic media is the safer call.
- Ignoring compound chemistry. Unbalanced compound glazes media and leaves residue that ruins downstream plating.
- Skipping separation design. If parts and media cannot be split quickly, labour savings evaporate at unload.
- Buying before sampling. Size the machine to a verified trial cycle, not to a sales sheet.
Frequently Asked Questions
What is the difference between mass finishing and vibratory finishing?
Mass finishing is the umbrella term for batch surface treatment using media. Vibratory finishing is one method within it, alongside barrel tumbling, centrifugal disc, and drag finishing. All are mass finishing processes.
How long does a mass finishing cycle take?
Light deburring typically takes 15–30 minutes. Heavy stock removal or a bright cosmetic finish can run several hours. Material, burr size, media, and finish target all move the clock.
Can mass finishing damage delicate parts?
It can if you use the wrong media or too much energy. Plastic media at low amplitude is very gentle, and drag finishers isolate parts entirely so they never strike each other.
Is wet or dry mass finishing better?
Wet is standard for deburring and polishing because the compound lubricates, cleans, and prevents rust. Dry processes suit specific polishing steps or where water is undesirable.
How do I choose between a bowl and a tub machine?
Choose a bowl for small-to-medium parts that need strong circulation and easy unloading. Choose a tub for long, large, or fixtured components that will not sit well in a round bowl.
Conclusion
A mass finishing machine is the most cost-effective way to deburr, radius, descale, and pre-polish metal parts in volume. Match the configuration to your part geometry, select media for your alloy and finish target, and run a sample batch before you commit. If you are planning a new line or upgrading manual finishing, our team can size a turnkey system to your throughput — send us parts and we will return a verified cycle time and quotation.