Faucet Production Cost: How Automation Lowers per Unit
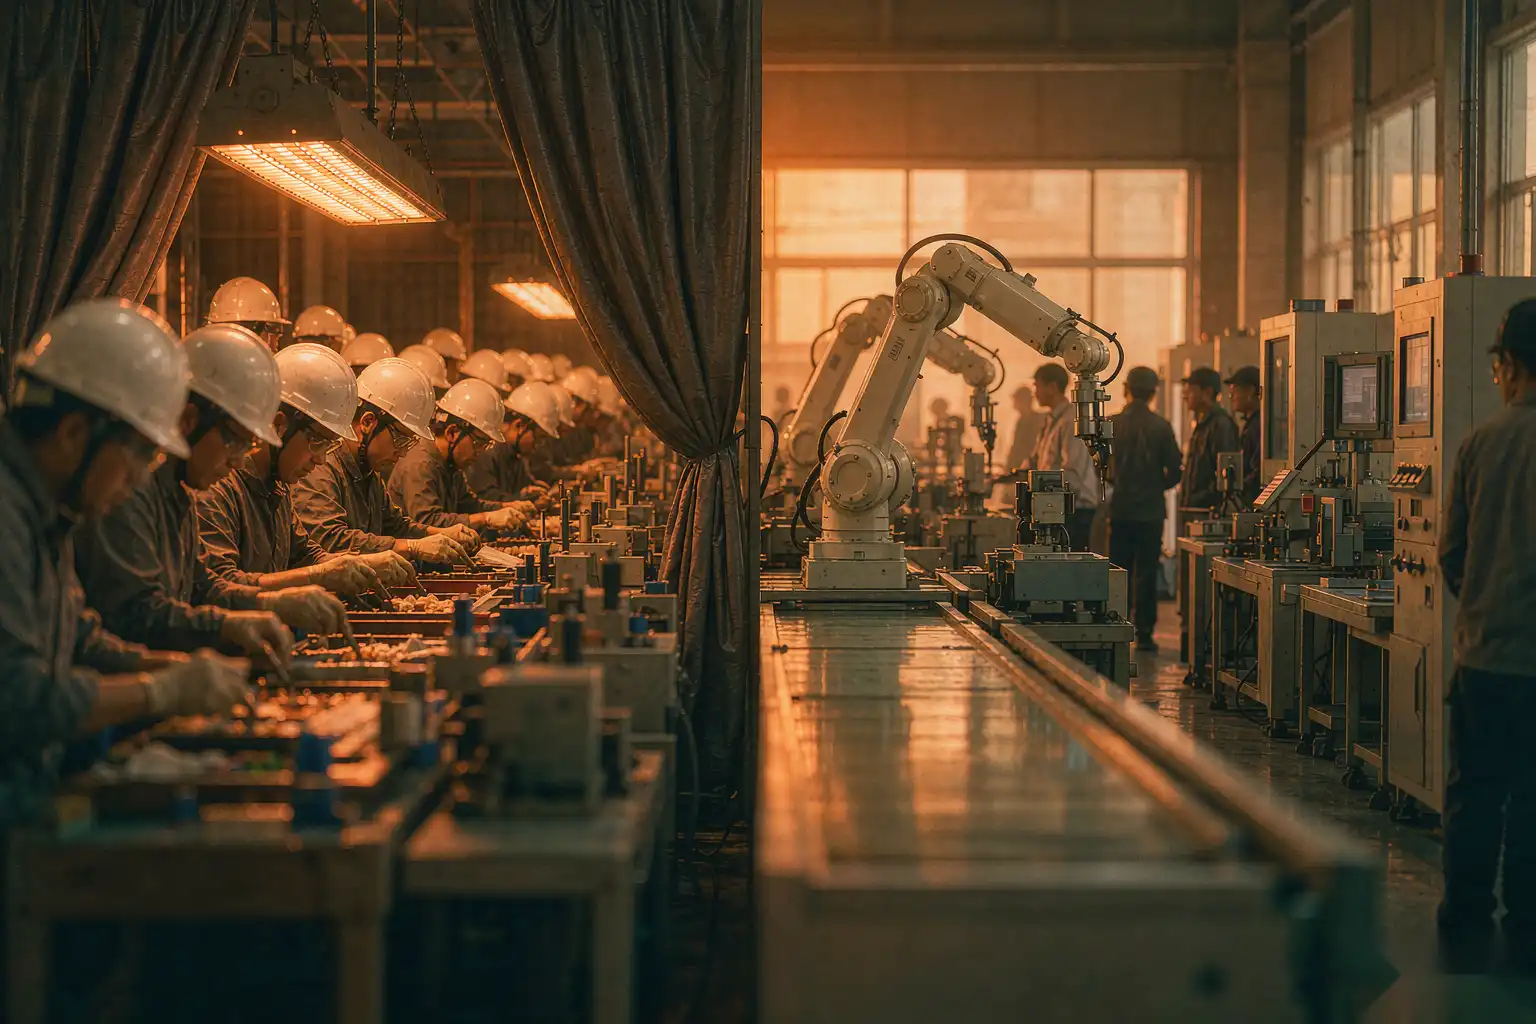
A faucet maker in Mexico showed us two cost sheets for the same part: one hand-finished, one from an automated line. The metal was identical. The difference in per-unit cost was almost entirely labor, scrap, and rework. “Automation isn’t about buying a robot,” he said. “It’s about removing the cost that walks out the door every shift.” That’s the right way to read faucet production cost.
This guide shows where automation actually cuts per-unit cost, and where it doesn’t.
What Drives Per-Unit Faucet Cost
Three things dominate the cost of a finished faucet body: direct labor per part, scrap and rework, and consumable waste (belts, wheels, plating bath). Automation attacks all three, but not equally, and not all at once.
Where Automation Pays Back First
Labor is the most visible saving. A hand grinder and buffer finish a few dozen bodies an hour; a cell finishes hundreds with one operator supervising several. Scrap falls next, because locked programs don’t have a bad-day variance. Consumables drop when belts and wheels are managed by the cell instead of changed on guesswork.
Our station automation guide shows which steps to automate in what order to reach a balanced line.
The Cost Levers That Matter
Labor per Part
Automation converts labor from per-part to per-line. One supervisor covers casting, CNC, grind, buff, and plate. The per-unit labor line drops with volume.
Scrap and Rework
Inconsistent hand finishing means a slice of bodies get reworked or scrapped. Consistent cells cut that slice sharply, and scrap is purchased alloy thrown away. The locked-recipe levers are the same ones that cut foundry scrap in die casting automation
Consumable and Energy Control
A managed cell uses belts, wheels, and bath efficiently. Unmanaged manual finishing wastes both. The saving is small per part but real across a year.
Three Mistakes Buyers Make
1. Counting only the machine price. Per-unit cost is what you compete on. Compare total cost per finished body, not robot sticker price.
2. Automating the wrong station first. Automate the bottleneck, not the easiest cell. A fast CNC behind a slow hand-grind still ships at grind speed.
3. Ignoring scrap in the payback. Scrap reduction is often the largest, least-talked-about saving. Put it in the model.
Frequently Asked Questions
How fast does faucet line automation pay back?
It depends on volume and current scrap, but labor and scrap savings usually dominate. At steady volume with high rework, payback often lands in well under two years; confirm against your own cost sheet.
Does automation raise quality cost or lower it?
It lowers per-unit cost because consistent parts need less rework and fewer consumables. The first bodies out of a cell cost the same as the ten-thousandth, which manual finishing can’t promise.
Should I automate all stations at once?
Not necessarily. Automate the bottleneck first, prove the saving, then extend. A phased line still needs a balanced takt target so later stations don’t strand the gain.
This guide was prepared by the application engineering team at Xiamen Dingzhu Intelligent Equipment Co., Ltd. (DZ Machinery), which designs and commissions deburring, grinding, polishing, and die-casting lines for manufacturers across more than a dozen countries. Cost figures are directional; model your own labor, scrap, and volume before purchase.
Tags: faucet production line, automatic faucet production, faucet manufacturing, automation, finishing cost, automation ROI