Turnkey finishing line cost questions start where single-machine pricing ends. A line is a system, and its price follows station count, integration depth, and the engineering required to make independent machines behave as one flow. This article walks the whole build.
We break the line into stations with real cost ranges, map the build sequence from contract to production, and name the risk areas where line projects most often slip. Use it to scope your project before requesting quotes.
What Turnkey Actually Includes
Turnkey means one supplier owns the outcome rather than the components. They deliver engineering, machines, integration, installation, commissioning, and training under one contract. You get a single number and a single throat to choke.

The alternative, self-integration, buys stations separately and manages connections in-house. It can cost fifteen to twenty-five percent less on paper. It also absorbs your engineering team for months and moves integration risk onto your schedule.
Choose turnkey when your team lacks integration experience or your timeline is tight. Choose self-integration when you have strong controls engineering and a genuine appetite for project management. Both are legitimate, and the wrong choice is expensive either way.
Station-by-Station Cost Structure
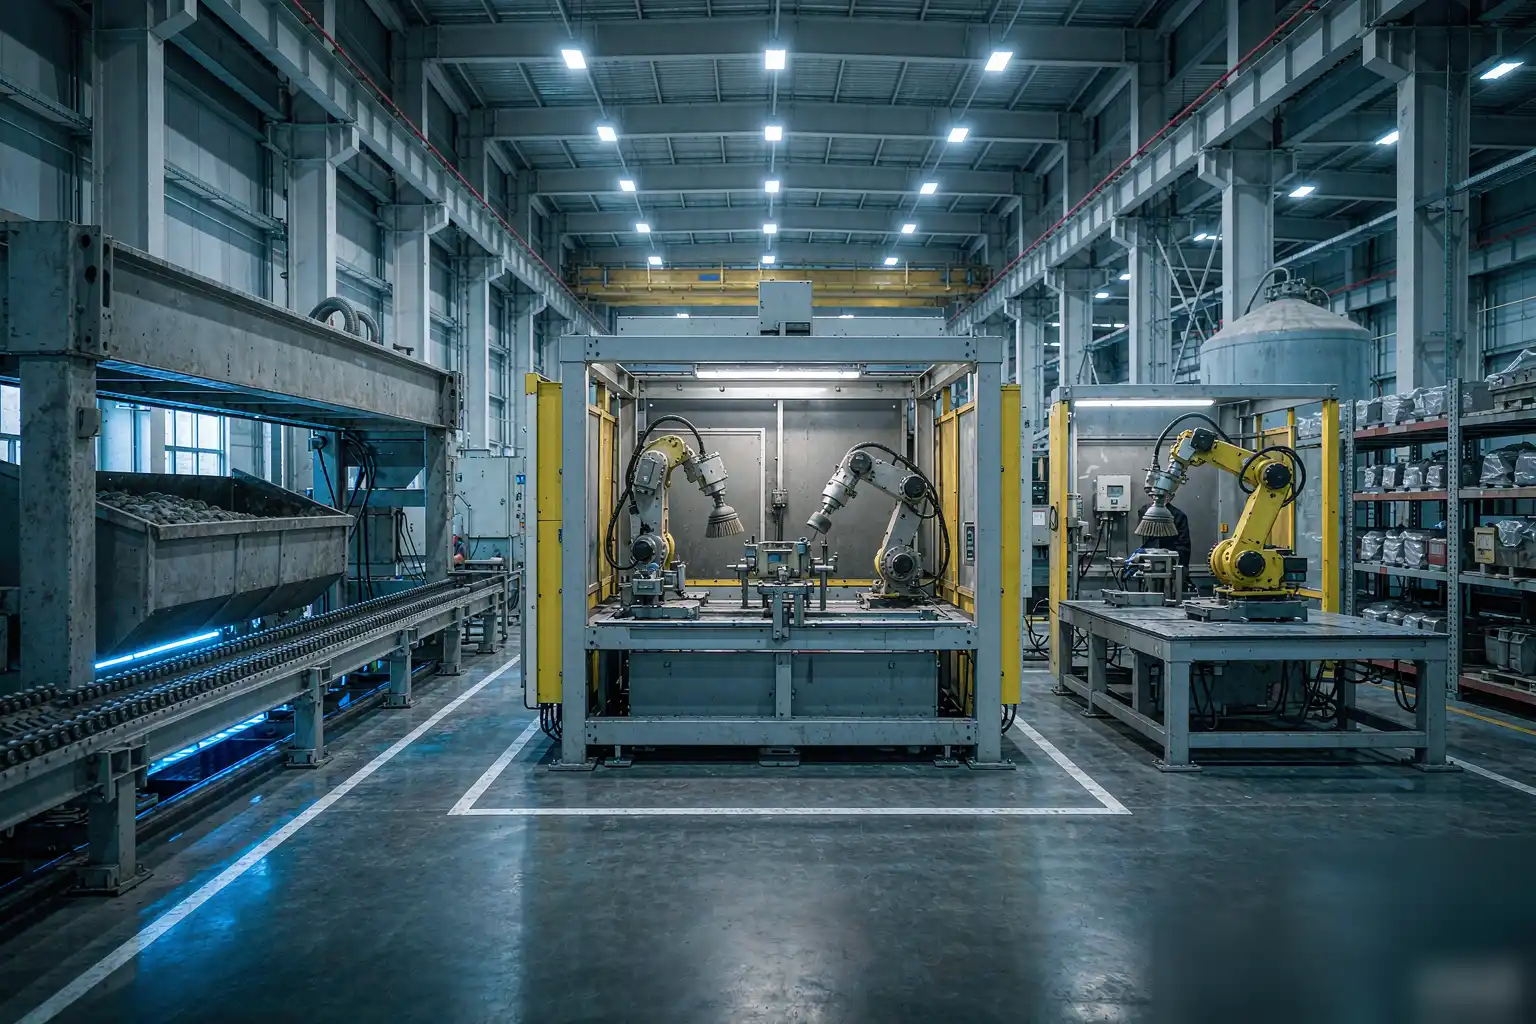
A line’s price is the sum of its stations plus integration. Here is the typical structure for a mid-volume casting finishing line, with ranges that reflect common configurations.
| Station | Cost Range | Function |
|---|---|---|
| Load and unload | $30k – $90k | Part presentation and buffering |
| Deburring | $80k – $220k | Parting lines, holes, edges |
| Rough grinding | $120k – $300k | Stock removal, seam leveling |
| Fine grinding | $100k – $260k | Surface preparation |
| Polishing or buffing | $150k – $400k | Final finish and color |
| Washing and drying | $60k – $150k | Compound and swarf removal |
| Inspection | $40k – $180k | Vision or manual verification |
| Material handling | $80k – $250k | Conveyors, transfers, buffers |
Total installed cost typically lands between 650,000 and 1,800,000 dollars. The spread reflects station count, automation level, and inspection sophistication. Lines for simple parts sit at the low end; cosmetic-finish lines run high.
The Integration Engineering Scope
Integration is where line projects earn or lose their schedule. It covers controls architecture, part tracking, error recovery, recipe management, and data collection. Expect it to run fifteen to twenty-five percent of total cost.
Controls Architecture
One supervisory controller should orchestrate the stations. Distributed control with peer-to-peer handshakes works but complicates troubleshooting. Insist on a clear architecture document before contract signing.
Part Tracking
Every part needs identity through the line, usually via fixture ID or RFID. Tracking enables per-part process history and makes quality investigations tractable. Retrofitting tracking later costs several times more than designing it in.
Error Recovery
Stations stop. The design question is what happens next. Good lines isolate a fault, hold upstream parts safely, and resume automatically. Poor lines require a full stop and manual restart, which destroys the throughput you paid for.
Recipe Management
Multi-part lines need recipe selection that operators cannot get wrong. Tie recipes to fixture ID rather than manual selection. The elimination of wrong-program errors alone justifies the engineering.
The Build Sequence
Turnkey projects follow a predictable sequence. Knowing the phases helps you staff them and hold dates. The timeline below reflects a typical eight to twelve month project.
| Phase | Duration | Your Team’s Role |
|---|---|---|
| Process definition and sampling | 4 – 8 weeks | Provide parts, define finish standards |
| Engineering and layout approval | 6 – 10 weeks | Review drawings, approve layout |
| Build and factory test | 12 – 20 weeks | Attend FAT, witness test runs |
| Shipping and installation | 3 – 6 weeks | Prepare floor and utilities |
| Commissioning and ramp | 6 – 12 weeks | Staff the line, run production parts |
| Acceptance and handover | 2 – 4 weeks | Verify against acceptance criteria |
Two phases deserve extra attention from your side. Factory acceptance testing is your last cheap chance to catch problems, so attend with your own parts. Commissioning is where training must actually happen, because classroom learning forgotten by week three helps nobody.
Commissioning in Three Sub-Phases
Commissioning is not one event. It runs dry, then wet, then productive. Understanding the sub-phases prevents the classic frustration of expecting production output during week one.
Dry Commissioning
Stations cycle without parts. Sensors verify, transfers time correctly, and safety systems prove themselves. Problems found here are cheap. Expect a week for a mid-size line.
Wet Commissioning
Parts enter the line, and programs get tuned station by station. Cycle times start long and improve daily. This phase generates the scrap you budgeted for, and generates most of the learning your team will keep.
Production Ramp
The line runs scheduled production with decreasing supervision. Throughput climbs toward target over four to eight weeks. Judge the line at the end of ramp, not at the end of wet commissioning, or you will be disappointed unfairly.
Plants that understand this sequence report far better project experiences. Our robotic grinding cell setup guide covers the same discipline at single-cell scale.
Where Line Projects Slip
Three risk areas cause most schedule slips and budget overruns. Each has a known mitigation, and each mitigation costs less than the risk.
Part Variation Beyond Samples
Sampling uses good parts. Production sends everything. Mitigate by sampling across batches and specifying compensation capability for the variation you actually see, not the variation you hope to see.
Utility and Site Readiness
Lines need power, air, water, drainage, and floor capacity that older buildings sometimes lack. Survey the site with the vendor’s utility sheet early. A late-discovered transformer requirement can cost weeks.
Scope Creep After Contract
Changes during build are expensive and slow. Freeze the part list and finish standards at contract. Additions are fine after handover, when the line is stable and change costs are normal.
Acceptance Criteria That Protect You
Acceptance is your leverage, so define it precisely before signing. Name the parts, the throughput rate, the finish standard, and the availability target. Then measure with instruments your inspectors already use.
| Criterion | Example Target | Measurement |
|---|---|---|
| Throughput | Parts per hour sustained | One full shift of production |
| Finish quality | Ra range on named surfaces | Your roughness instrument |
| Availability | Percentage of scheduled hours | Two weeks of logged runtime |
| Changeover | Minutes between part families | Timed live changeover |
Sustained rates matter more than peak rates. A line that hits target for one hour proves little. Require a full shift, and the number means something. For single-machine acceptance guidance, our robotic polishing machine comparison includes the contract clauses to demand.
Staffing the Line After Handover
A line needs people, just fewer of them. Plan for one operator per two or three stations, plus a technician who owns recipes, tooling, and first-line maintenance. Name that technician during commissioning, not after.
Our operator training guide for automated grinding and polishing lays out the four-week program that turns existing staff into line owners. Start it during commissioning, when the learning is contextual and retention is highest.
Deciding Whether a Line Is Right
Lines suit stable products at volume. They are poor fits for unstable designs, wide mixes, or volumes too low to keep stations busy. Be honest about your product maturity before signing a line contract.
If maturity is uncertain, buy cells first and connect them later. Cells become stations when you are ready, and the modular route forgives uncertainty that a line cannot. Factories that grow this way rarely regret the sequencing.
Data Infrastructure Worth Building In
Modern lines generate enormous process data. Capturing it during build costs far less than retrofitting afterwards, and the data pays for itself during the first quality investigation.
Log cycle times, station-level reject counts, and consumable changes per part. These three streams answer most production questions within minutes. Add force and power traces per cycle if your budget allows, because those predict tool wear before quality drift appears.
Decide the data destination early. Whether the line reports to a local historian or your MES, define the interface during engineering rather than discovering it during commissioning. Retrofitted interfaces cost several times more and always arrive late.
The Number That Matters
Turnkey finishing line cost is a system price, and system prices reward clarity. Define the stations you need, budget integration honestly, prepare the site early, and write acceptance criteria before the contract exists.
Do that, and the line arrives on schedule at the agreed number. Skip it, and the project teaches you the same lessons at several times the price. The choice is genuinely yours, and it is made during scoping, not during build.
Scope carefully, staff the phases, and hold acceptance criteria that name your parts and your standards. Do that and a turnkey line becomes the most predictable capital project in your plant rather than the most stressful one.
Revisit the station list every year after handover. Product mixes shift, and the bottleneck station changes with them. Lines that get reviewed evolve gracefully; lines that get ignored quietly become the constraint nobody wants to discuss.
Begin with the process definition phase, and resist pressure to compress it. Every week spent there removes two weeks from commissioning, and the savings compound through the entire build.
Tooling and compound choices should be confirmed against your alloy and finish target.