


Aluminum Die Casting Tooling: Die Design, Materials, and Lifecycle Management
Why the Die Is the Most Important Decision
The die (the steel tool that shapes the part) is the single most important factor in die casting economics and quality. The die determines:
- Part quality — surface finish, dimensional accuracy, defect rate
- Cycle time — how fast parts can be produced
- Tooling life — how many parts the die produces before refurbishment
- Maintenance cost — ongoing die care and repair
- Flexibility — how easily the die can be modified for engineering changes
A well-designed die pays for itself many times over. A poorly designed die creates a chronic quality and cost problem.
Die Design Basics
Single-Cavity vs Multi-Cavity
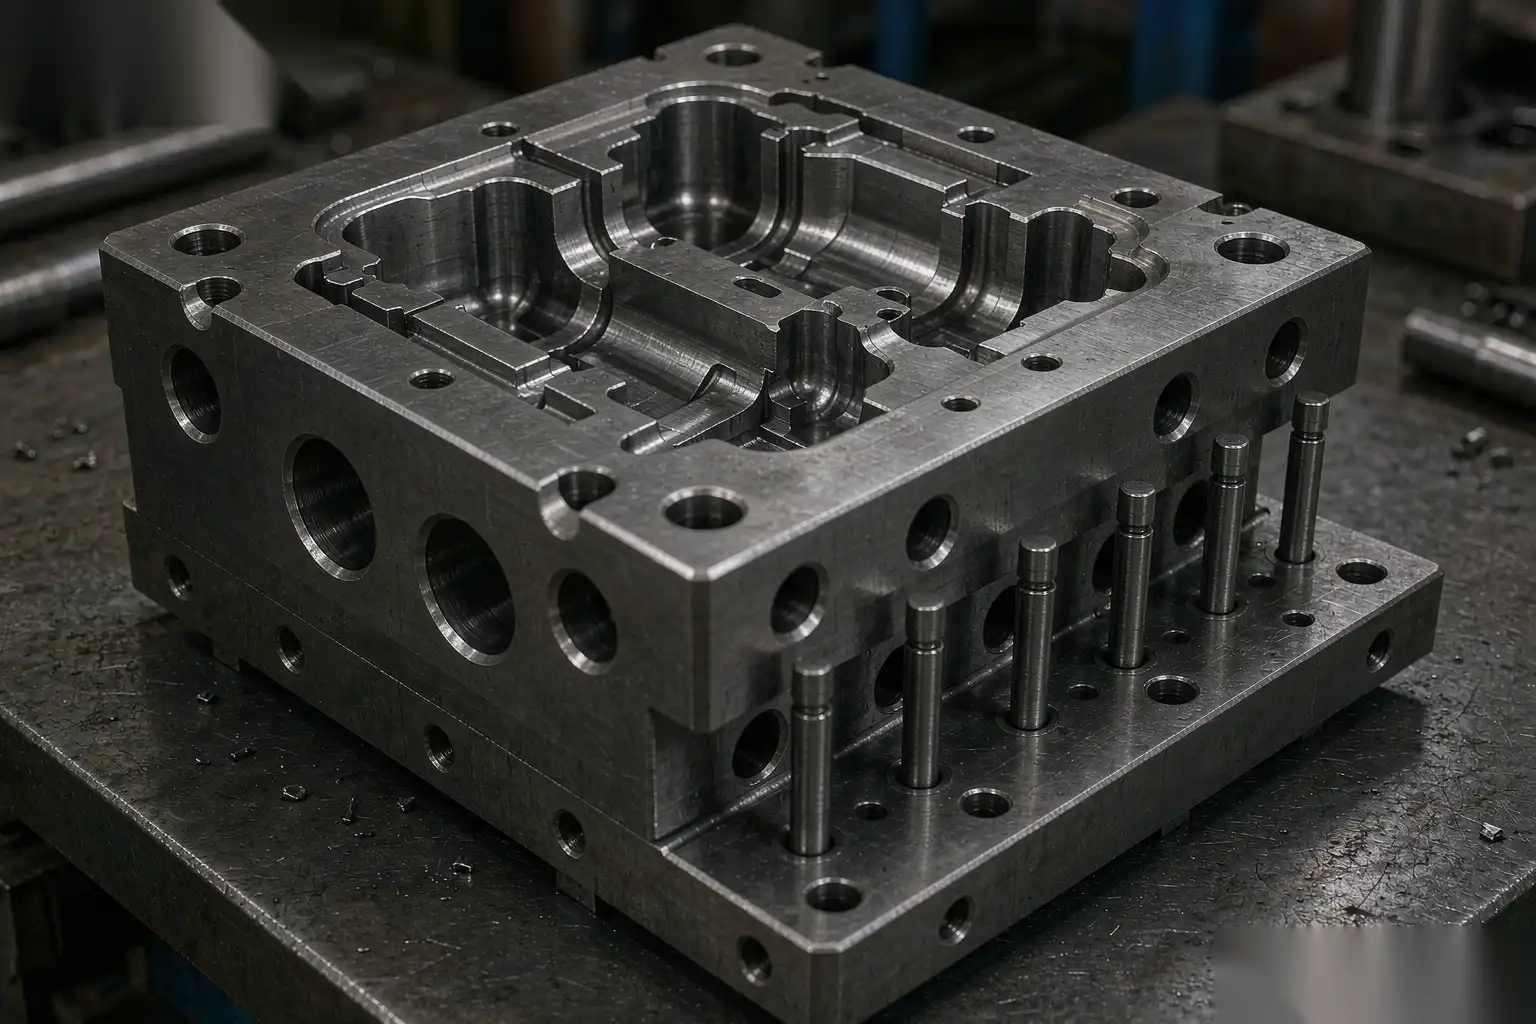
- Single-cavity die: one part per cycle. Lower tooling cost, longer cycle time per part. Best for large parts, low volume, or when cycle time is not the constraint.
- Multi-cavity die: 2, 4, 8, or more parts per cycle. Higher tooling cost, shorter cycle time per part. Best for small parts, high volume, or when production rate is critical.
The breakeven is typically around 50,000-100,000 parts/year. Below that, single cavity is usually cheaper. Above that, multi-cavity pays back the higher tooling cost.
Parting Line
The line where the two die halves meet. Determines:
- Flash location — flash always occurs at the parting line
- Cosmetic appearance — parting line witness is often visible
- Trim die design — affects the trim die complexity
- Gate location — the gate is usually at or near the parting line
The die designer chooses the parting line, but you should review the proposal. Look for:
- Parting line on a non-cosmetic surface (or a surface that can be hidden by a gasket or trim)
- Even draw on both die halves
- Minimal undercuts
- Easy access for trim die
Gating System
The channel through which molten aluminum enters the cavity:
- Gate type: tab gate, fan gate, ring gate, or sprue gate
- Gate location: should fill the cavity with single front (no converging flow)
- Gate thickness: 0.8-2.5 mm depending on part size
- Overflow wells: at the end of the fill path to capture cold metal and air
- Vents: at the end of the cavity to allow air to escape
Poor gating causes 50%+ of all die casting defects. The gate design is the single most important factor in defect reduction.
Cooling System
The channels through which water or oil flows to control die temperature:
- Cooling channels: typically 8-15 mm from the cavity surface
- Coolant: water (most common) or oil (for high-temperature areas)
- Baffles and bubblers: for cooling deep cavity features
- Conformal cooling: 3D-printed cooling channels for complex cavities (emerging technology)
- Cooling balance: even cooling prevents warping and reduces cycle time
Poor cooling causes warping, hot spots, longer cycle times, and shorter die life. Thermal simulation during die design identifies hot spots and optimizes channel layout.
Ejection System
The mechanism that pushes the part out of the die after solidification:
- Ejector pins: the most common, used for most parts
- Ejector sleeves: for parts with internal features (bores, threads)
- Stripper plates: for parts with large surface area
- Knock-out pins: for parts that need positive ejection
Ejector pin design affects:
- Part surface quality — ejector pin marks are visible
- Part warping — uneven ejection force causes distortion
- Die life — ejector pins wear and need replacement
Tool Steel Selection
The die steel grade determines die life, cost, and capability:
| Steel Grade | Hardness (HRC) | Die Life (shots) | Cost | Use Case |
|---|---|---|---|---|
| P20 (pre-hardened) | 30-36 | 50,000-150,000 | low | low-volume, prototype |
| H11 | 48-52 | 100,000-300,000 | medium | standard die casting |
| H13 | 48-52 | 100,000-500,000 | medium-high | most common die casting steel |
| W302 (high-H13) | 50-54 | 300,000-1,000,000 | high | high-volume production |
| Dievar (Uddeholm) | 50-54 | 500,000-1,500,000 | very high | premium high-volume |
| Aluminum die (mild steel) | — | 1,000-5,000 | very low | prototype only |
Standard recommendation: H13 tool steel, hardened to 48-52 HRC, with nitrided or coated cavity surface for additional wear resistance. This gives the best balance of cost, life, and capability for most projects.
For high-volume projects (1M+ parts/year): W302 or Dievar extends die life and reduces refurbishment cost.
For prototypes or low-volume: P20 pre-hardened is cheaper and faster to machine, with acceptable life for 50,000-100,000 parts.
Cavity Surface Treatment
After machining, the cavity is often treated to improve wear resistance and release:
- Nitriding: diffuses nitrogen into the surface to form hard nitrides. Standard for die casting. Improves wear resistance and reduces galling.
- Chrome plating: hard chrome on cavity surface for wear resistance. Less common now due to environmental concerns.
- PVD coating: physical vapor deposition of TiN, CrN, or similar. Premium option for high-wear areas.
- Polishing: for cosmetic parts, the cavity is polished to mirror finish. Critical for visible parts.
- EDM texture: electrical discharge machining can create controlled textures for cosmetic appearance.
Die Fabrication Process
A typical die fabrication takes 4-8 weeks:
- Week 1-2: die design (3D CAD, simulations, design review)
- Week 2-4: rough machining (steel blocks machined to near-net shape)
- Week 4-5: heat treatment (hardening and tempering)
- Week 5-6: finish machining (cavity and core machining to final dimensions)
- Week 6-7: surface treatment (nitriding, polishing, coating)
- Week 7-8: die assembly and tryout (first shot test)
A first-shot die is rarely perfect. Expect 2-4 sampling iterations (T0, T1, T2) to optimize the die.
Engineering Changes and Modifications
After first article, engineering changes (ECs) are almost always needed:
- Common ECs: add draft, change wall thickness, add fillet, modify gate location
- Cost of ECs: 5-15% of original die cost, depending on complexity
- Time for ECs: 2-6 weeks, depending on scope
- Best practice: include a 10-15% EC budget in the project plan
Trying to skip ECs by getting the design perfect on the first try usually costs more in the long run.
Die Lifecycle Management
A die is a long-term asset that needs ongoing care:
Preventive Maintenance
- Daily: clean die, lubricate ejector pins, inspect for damage
- Weekly: check water/oil flow, inspect cooling channels, verify alignment
- Monthly: deep clean, inspect for wear, calibrate sensors
- Annually: full die inspection, refurbish worn areas, replace ejector pins
Common Die Failures
- Erosion: molten aluminum wears away the cavity surface
- Soldering: aluminum sticks to the cavity, leaving pits
- Heat checking: thermal fatigue causes cracks in the cavity surface
- Cracking: stress concentrations cause cracks, often at corners
- Distortion: uneven heating/cooling warps the die
A well-maintained die can produce 500,000-1,000,000 parts before major refurbishment. A poorly maintained die may fail at 50,000 parts.
Die Storage
When the die is not in production:
- Climate-controlled storage (20-25°C, <60% humidity)
- Anti-corrosion treatment on all exposed surfaces
- Documented storage location with clear identification
- Periodic inspection during storage to catch corrosion
Cost Structure of Die Casting Tooling
For a typical H13 tool steel die:
- Design and engineering: 10-15% of cost
- Steel material: 15-25% of cost
- Machining: 35-45% of cost (largest single component)
- Heat treatment: 5-10% of cost
- Surface treatment: 5-10% of cost
- Assembly and tryout: 5-10% of cost
Cost by die type:
- Single-cavity simple die: $15,000-40,000
- Single-cavity complex die with slides: $40,000-100,000
- Multi-cavity die (2-4 cavities): $60,000-200,000
- Large structural part die: $100,000-300,000+
These costs are for typical Chinese suppliers. Western suppliers typically charge 2-3x more.
Common Tooling Mistakes
In our experience, the most common tooling errors:
- No DFM review before tooling — design frozen, die made, problems discovered too late
- Cheap steel grade — P20 when H13 is needed, leading to short die life
- Insufficient cooling design — long cycle time, hot spots, warping
- Poor gate design — fill problems, porosity, weld lines
- No EC budget — change orders cause budget overruns and schedule slips
- No maintenance plan — die fails prematurely due to poor care
- Single-source tooling — no backup if the tool shop has problems
A well-managed tooling project avoids all of these.
What a Good Die Maintenance Program Looks Like
Die life is not decided by steel grade alone; it is decided by what happens between runs. A maintenance program worth the name has four visible marks, and all four are checkable during a supplier visit. First, a written log per die: shots accumulated, cleaning dates, nitriding dates, weld repairs with locations, and ejector pin replacements. If the shop cannot produce the log in five minutes, the program does not exist. Second, scheduled cavity cleaning and nitriding intervals tied to shot counts, not to failures — a die that gets re-nitrided every 50,000 shots ages on schedule, while one re-nitrided after soldering appears has already lost surface hardness where it mattered. Third, controlled storage: racks, identification, corrosion protection, and a checklist executed at both insert and removal. Fourth, water circuit verification on every maintenance cycle, because a partially blocked cooling channel silently lengthens cycle time and cooks one corner of the cavity long before anyone notices.
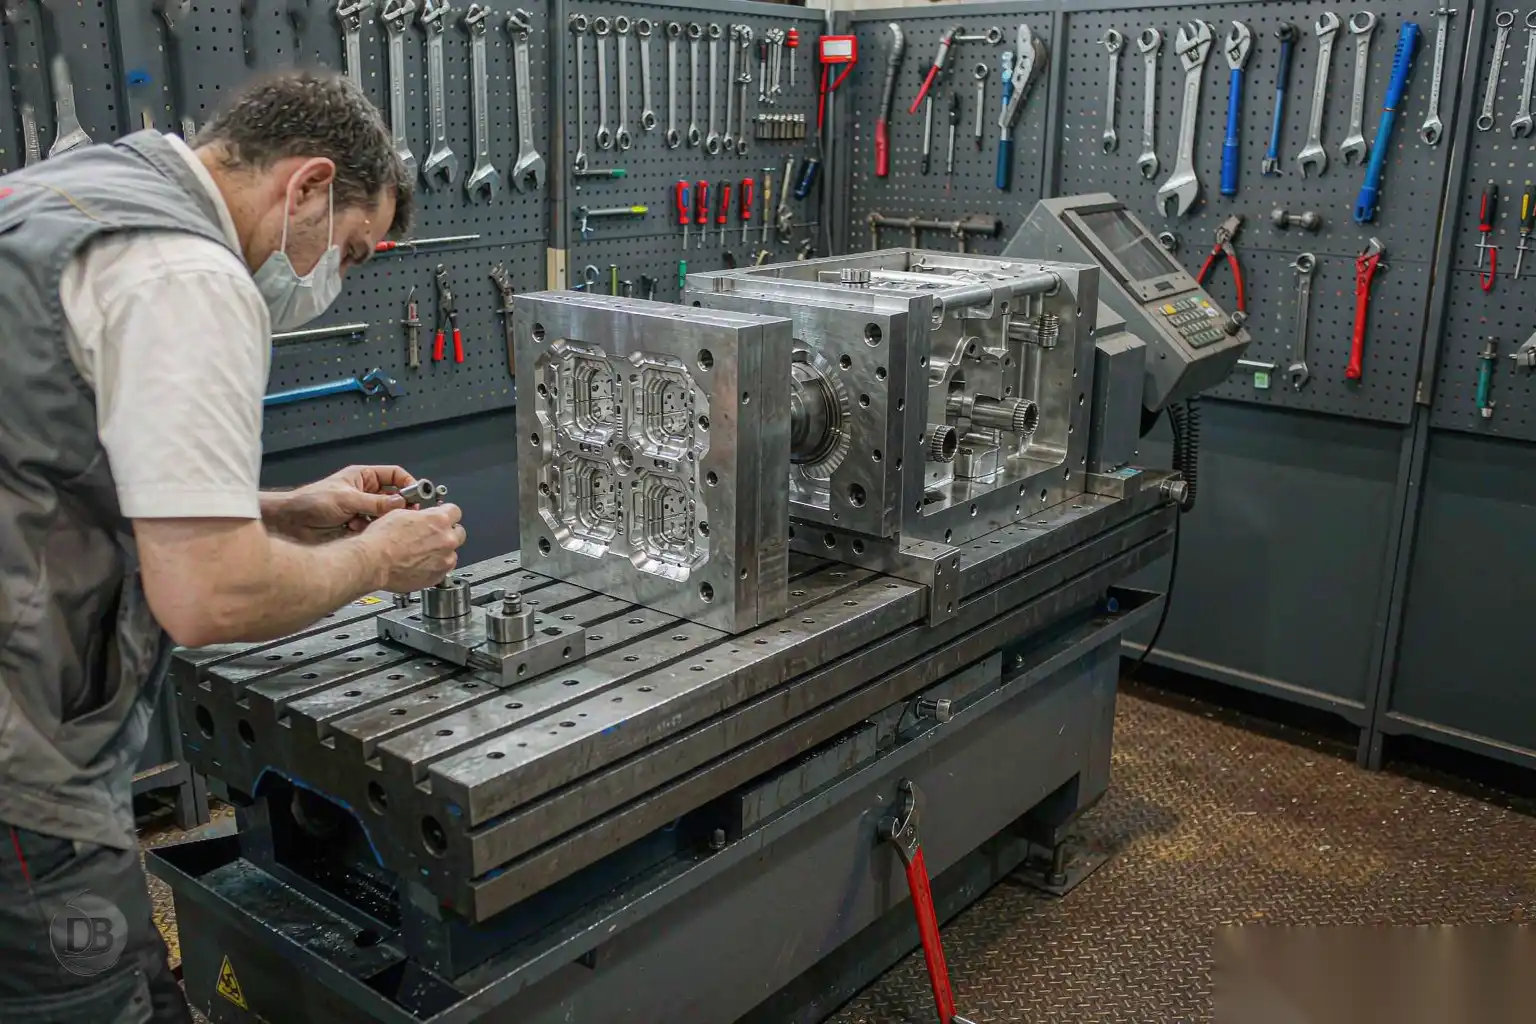
Ask to see the maintenance area itself. Dies opened up on benches, pins laid out in trays, measuring equipment at hand — that is a shop that owns die health. A warehouse of sealed crates with no records is a shop that owns die failures.
The finishing connection is direct: die condition is visible in the casting’s parting line, flash weight, and surface texture, and all three land in the deburring cell’s workload. DZ Machinery’s robotic cells hold their programs best on castings from shops with real die maintenance, because consistent flash means consistent material removal means stable cycle time. If your finishing costs are drifting upward quarter by quarter, ask to see the die logs before you retune anything else.
FAQ About Aluminum Die Casting Tooling
How long does it take to make an aluminum die casting die?
Plan 6-10 weeks for a typical single-cavity die: 1-2 weeks for design, 4-6 weeks for fabrication, 1-2 weeks for sampling. Complex dies with slides and multi-cavity configurations can take 10-14 weeks.
What is the typical die life for aluminum die casting?
H13 tool steel with proper maintenance produces 100,000-500,000 parts. Premium steels (W302, Dievar) can reach 1,000,000+ parts. Die life depends on the alloy (A380 is easier on dies than A390), the part geometry, the process parameters, and the maintenance.
Can the die be modified after it is made?
Yes, but at a cost. Engineering changes (ECs) after first article typically cost 5-15% of the original die cost and take 2-6 weeks. Common ECs include adding draft, changing wall thickness, modifying gate location, and adding or removing slides.
Should I buy the die from the same supplier that does the casting?
Usually yes, but not always. A die shop that does not operate its own die casting machines may not understand the process as well. On the other hand, a die caster that does not have a strong in-house tool room may outsource the design or fabrication, which can lead to communication problems. The best situation is a die caster with a strong in-house tool room and direct experience with the type of part you are making.
Building a Die that Lasts
A die is a long-term investment. The decisions you make in the design and fabrication phase determine the die’s life, the part quality, and the total cost of ownership over the die’s life.
At DZ Smart Manufacturing, our team has experience with die design, alloy selection, and process optimization for aluminum die casting. If you are starting a new project and want feedback on the tooling design, alloy choice, or process parameters, our engineering team can review your part spec and provide practical recommendations.
See our die casting support and automated finishing solutions



